Engineering Undertakings
A sample of the work we've delivered across management, manufacturing, mechanical engineering, R&D, product design and more.
Easton Technical Products
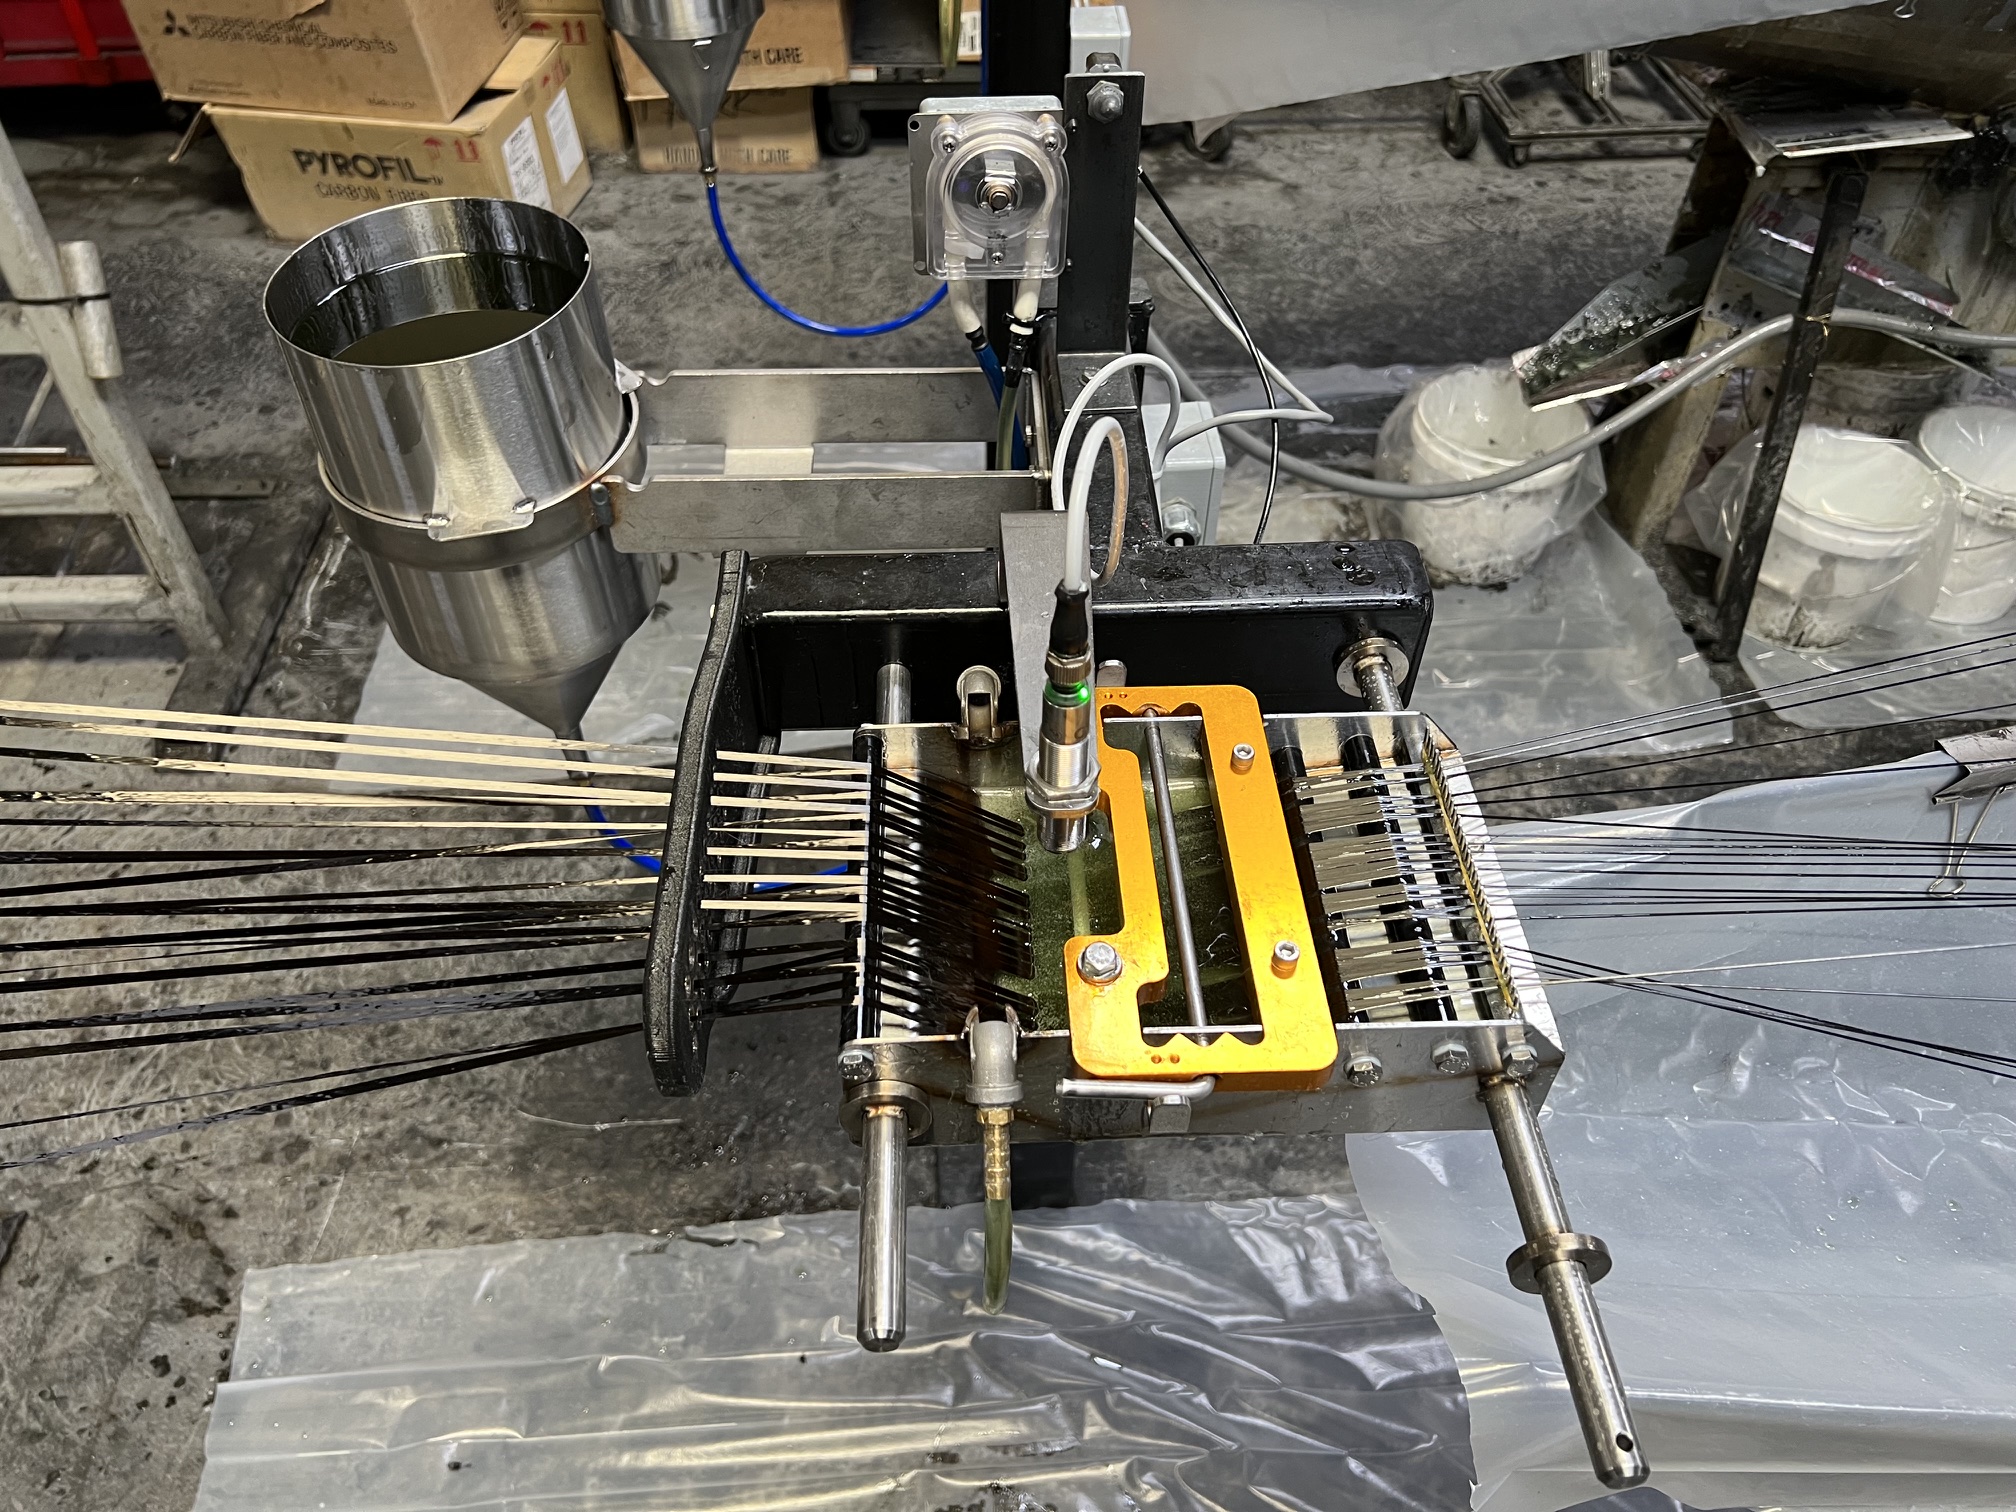
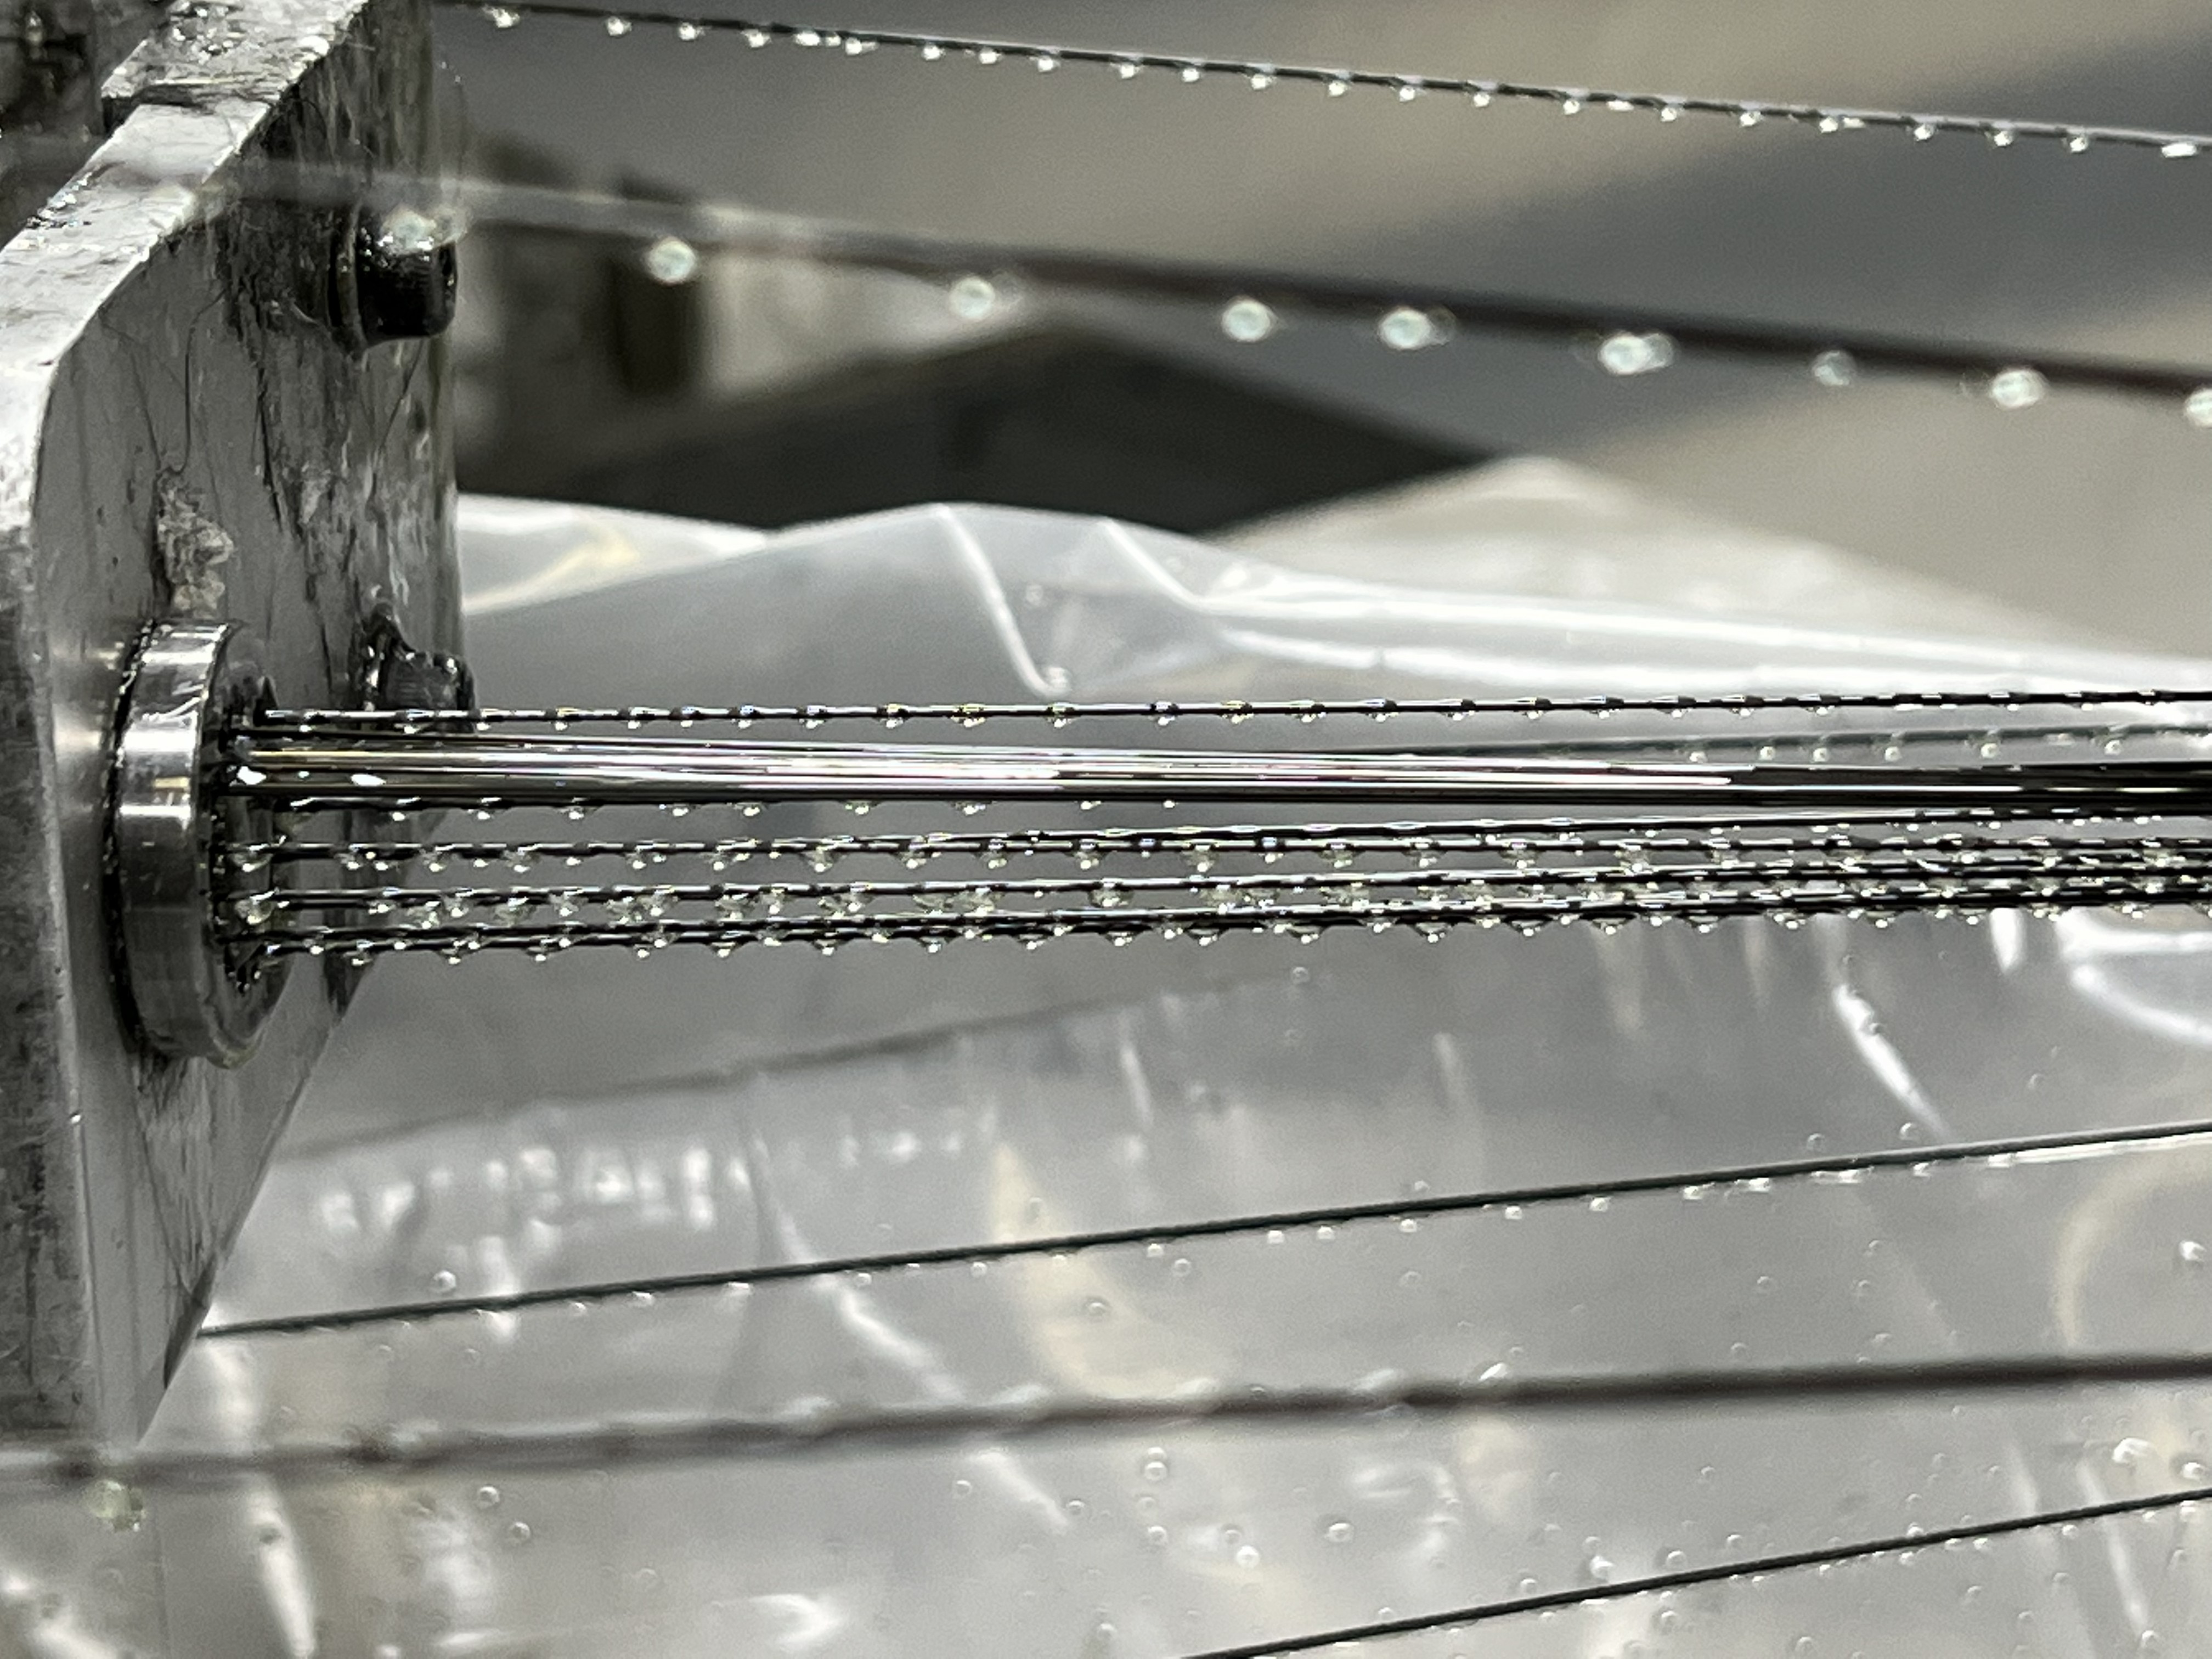
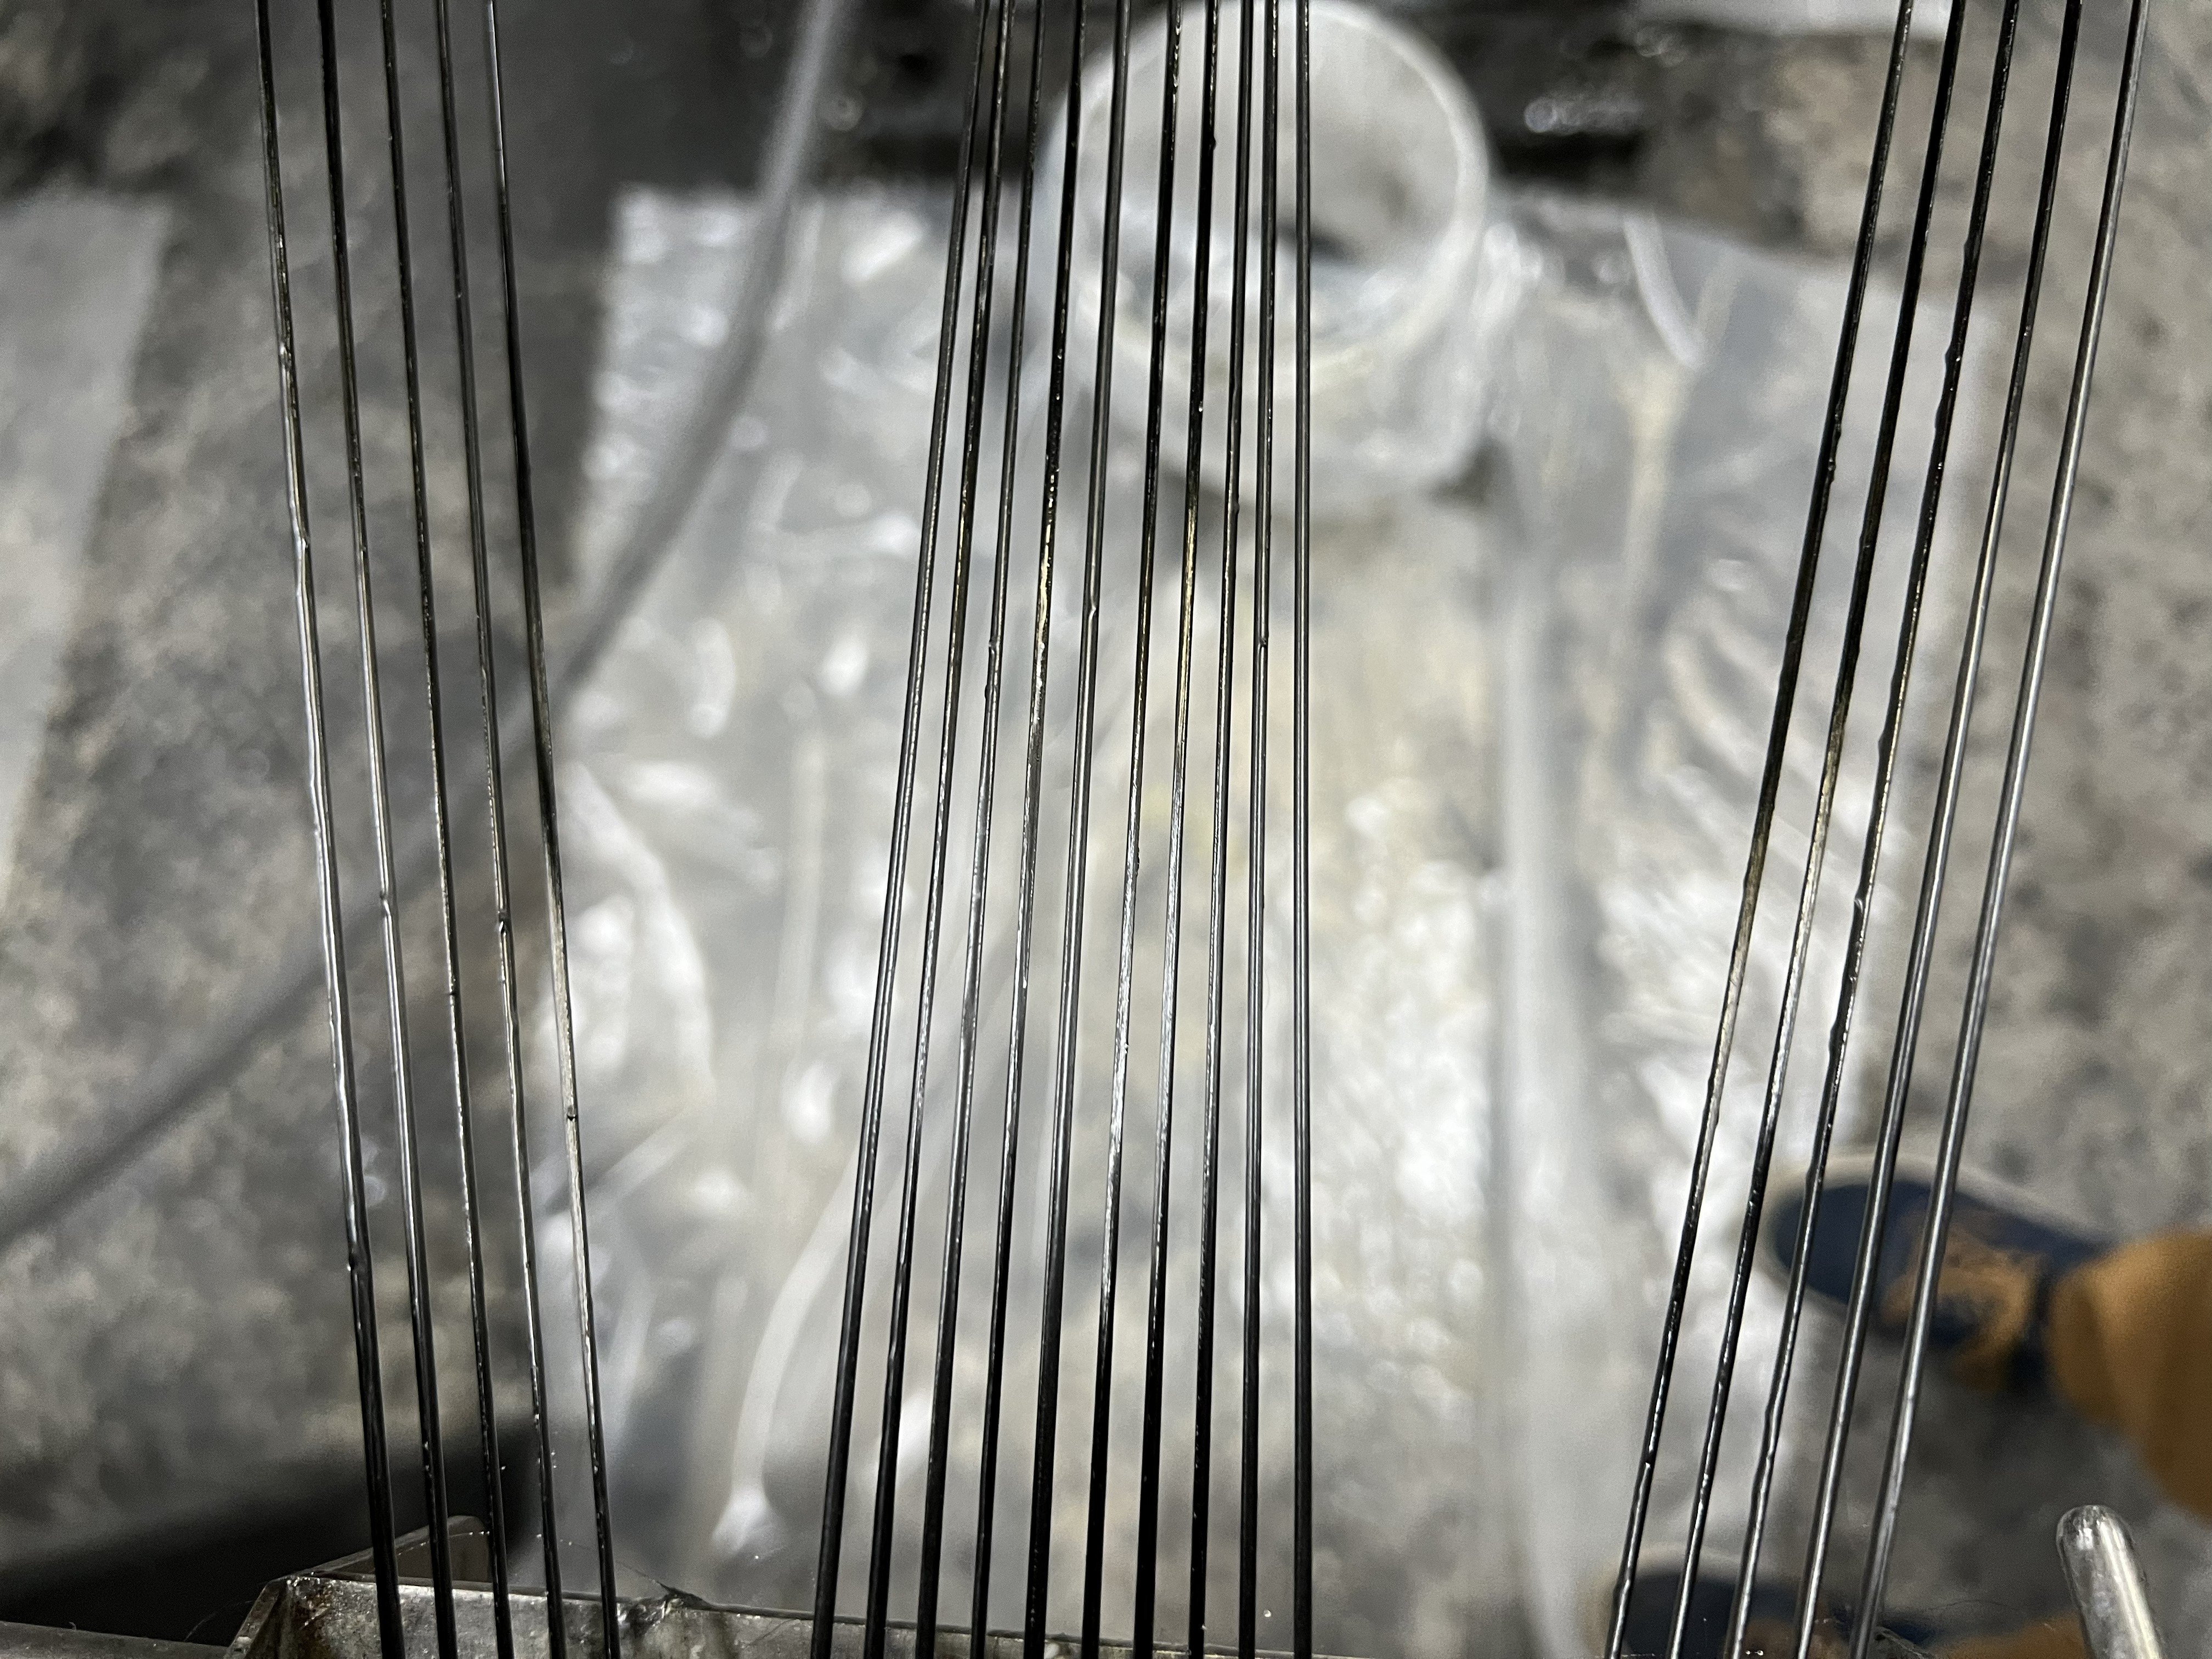
Easton makes composite archery shafts and tent poles via pultrusion. We designed a new impregnation process for the line from the ground up, replacing the existing method for wetting out the composite fiber as it's pulled and cured.
The new process cut material consumption in half while producing a stronger more resilient product. Because the plant runs 24 hours a day, the entire project paid for itself in one week.
Special thanks to Tyson Yates (VP of sales at Easton) and Josh Jones at Podium Archer for recently creating a video and showing the world what composite pultrusion can do. Check out the full factory tour video here on YouTube
More projects
Project management & coordinating
We have had multiple clients over time that needed guidance as far as team building and interim management for their engineers. We can advise on hiring structure/process, how to find good candidates for your specific roles, and coach you on how to think outside the box when searching for someone with niche skills etc. With our network of people in the industry we have a deep understanding to the ground level when it comes to management style and how we create culture change within a business of all sizes.
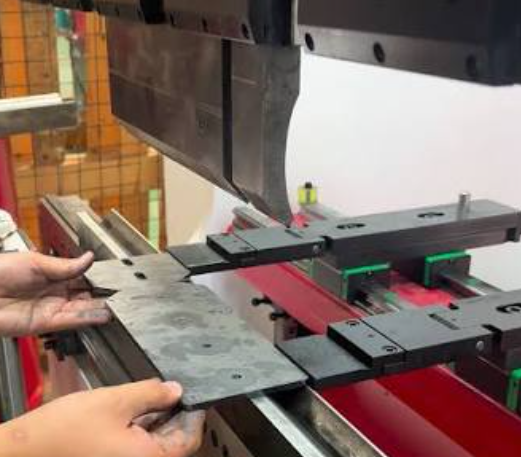
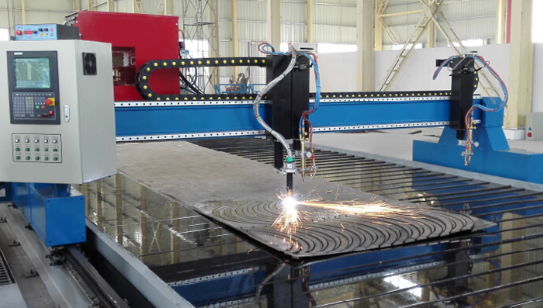
In the mechanical contracting world you may need Pre-fab solutions to create custom ductwork, run batches of plumbing or pipefitting. We have you covered with the ability to spec waterjets, laser tables, welders and other heavy equipment for your facility. We work with you every step of the way to ensure your system is capable of running the cycle time and appropriate duty cycle you need.
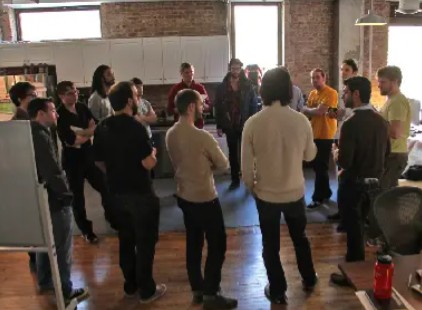
Through studying the workflow needs of Torus, we were able to determine they needed 52 individuals to run the 35000sq/ft facility at max capacity. We put together a hiring schedule to get there then began searching for production workers and tradesmen. We were able to grow the production team from 7 individuals to 19 in under 2.5 months while designing and building other workflows on the floor for them.
Process & flow improvement
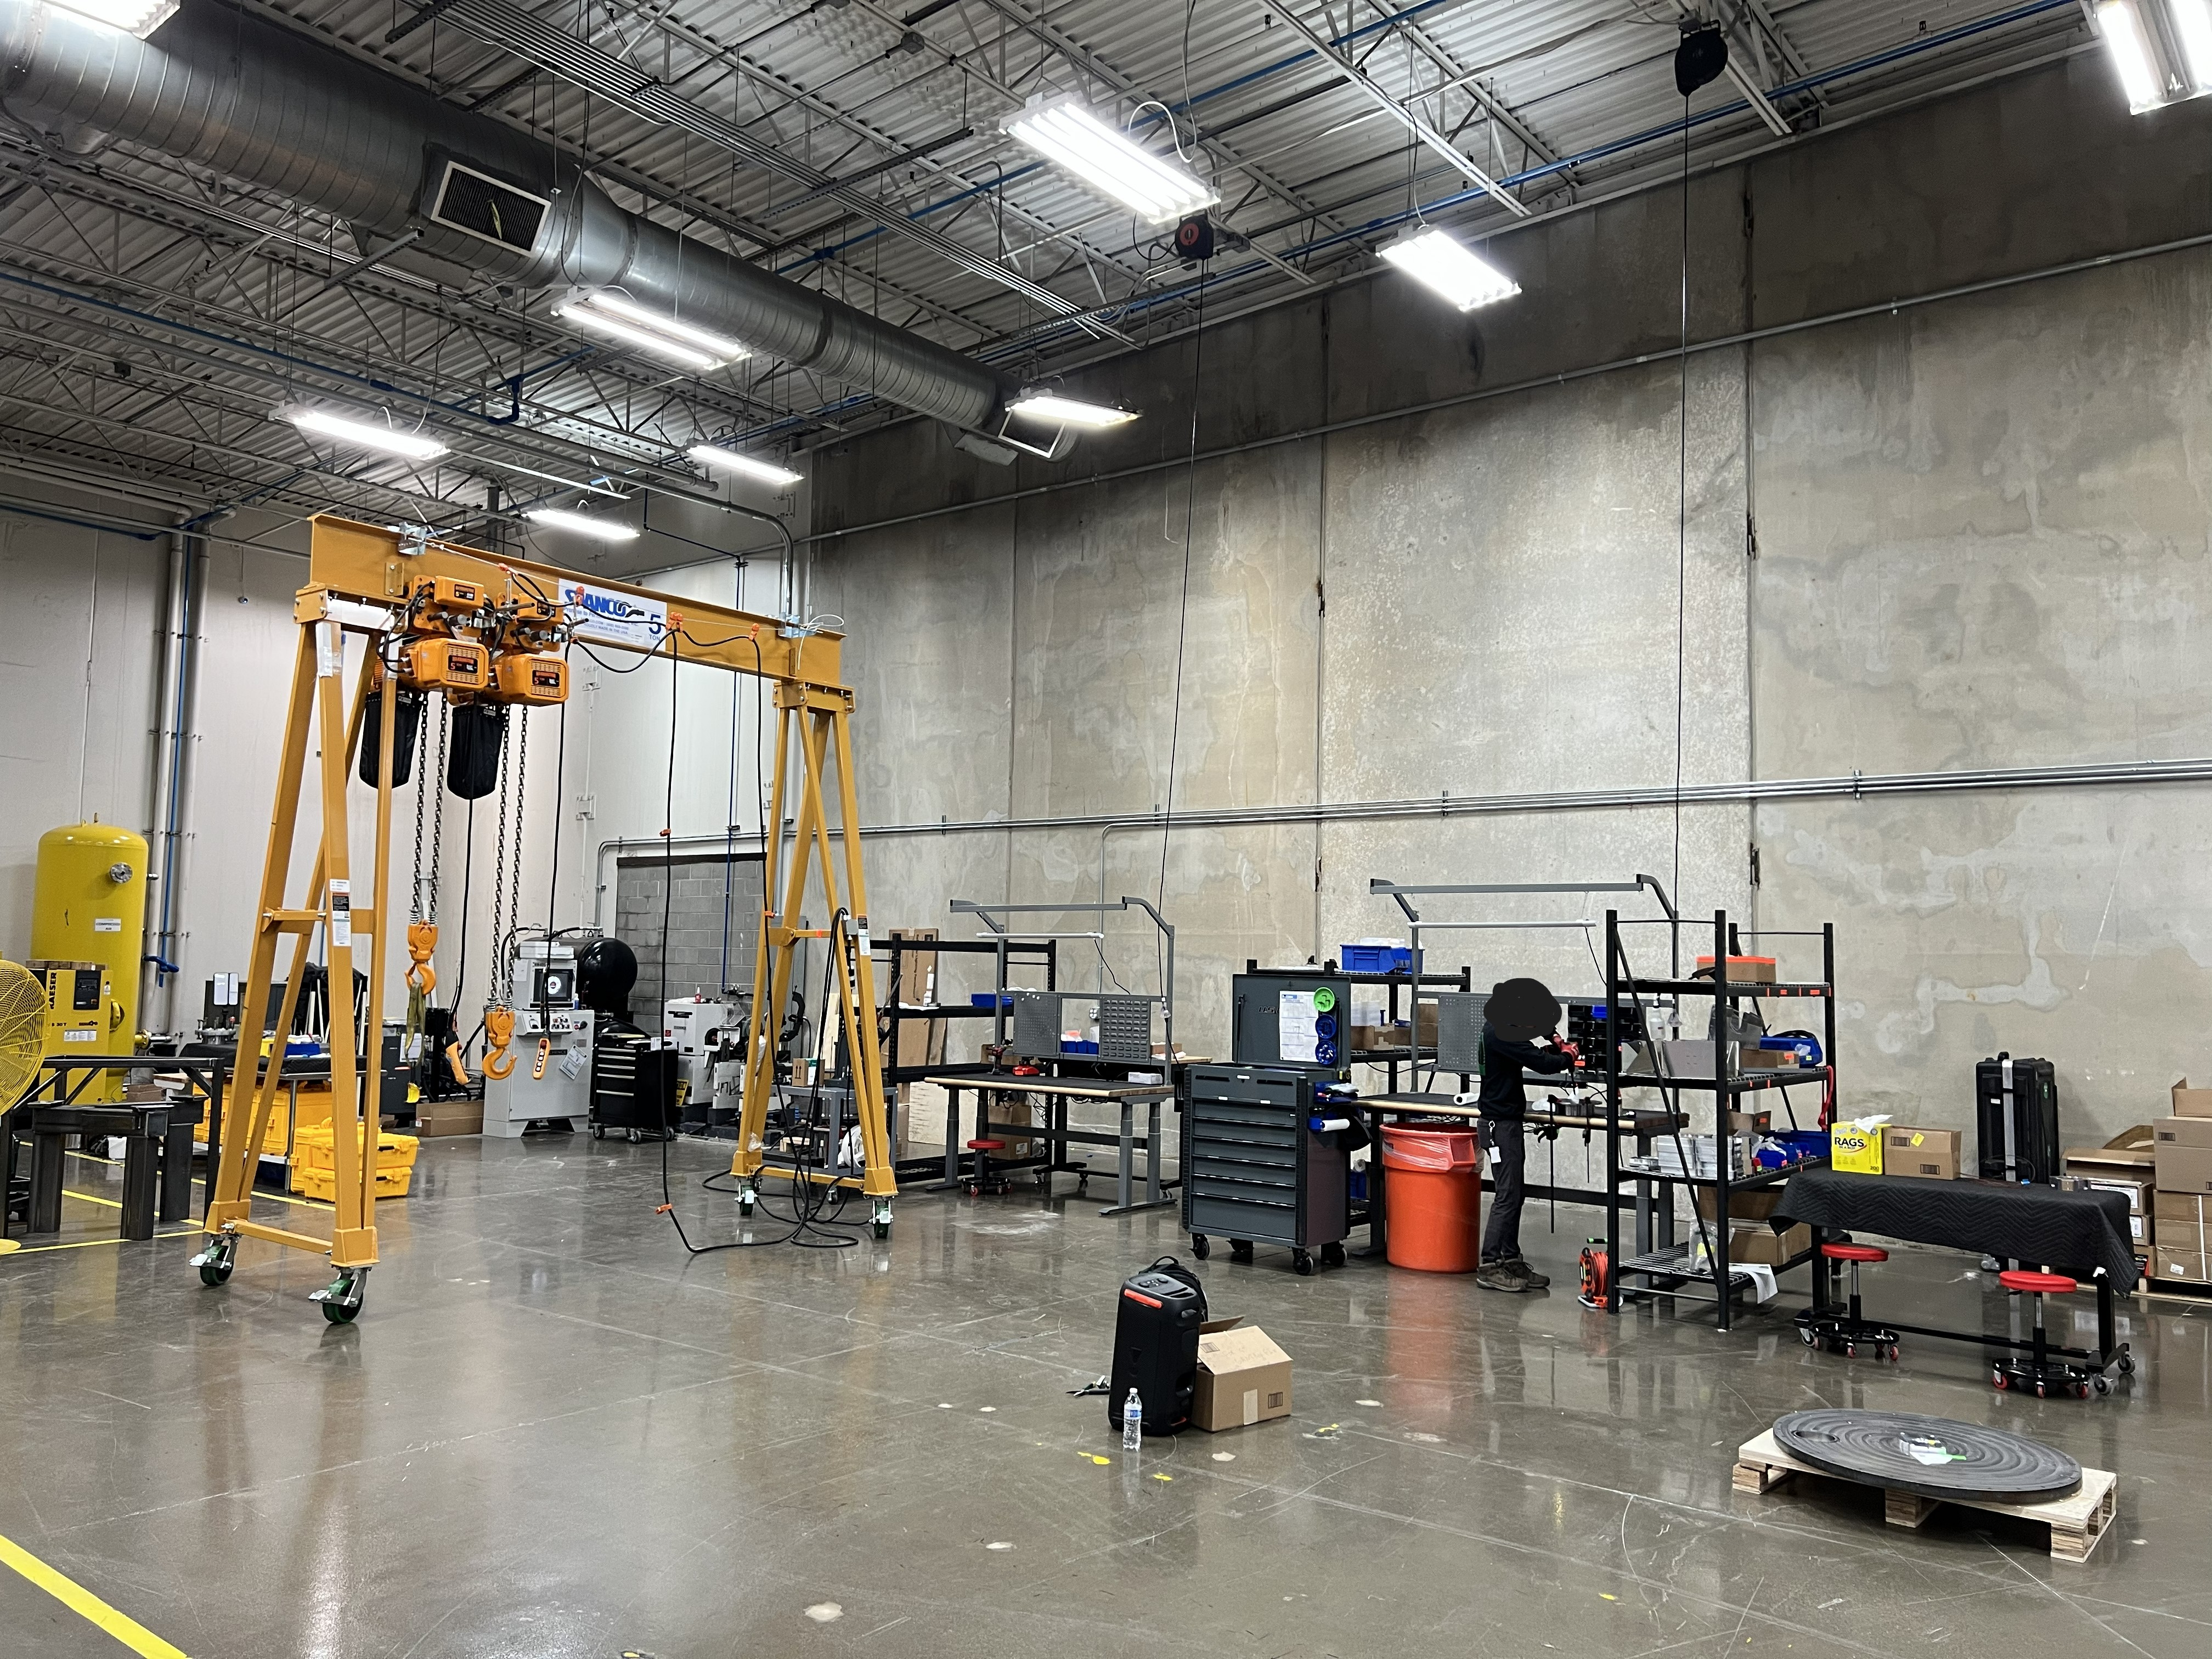
We went through the FESS area (Flywheel Energy Storage System) at Torus. From a flat floor we built a basic process flow for getting pre-fab parts and sub assemblies ready to go onto the finished product. My Engineer can handle anything from factory air systems to overhead cranes & custom built assembly stations and managing any percentage of the install for your assembly line design and build out.
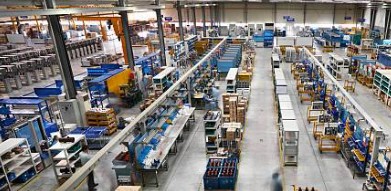
Client requested we build them a better process flow for electrical panel assembly covering a few variations. We handled the SOP's, floor layout, binning MAX/MIN limits, automatic wire stripper/cutter machines etc. Overall this was a great experience again to develop a system with all the input from the Existing employees and staff. It was a true pleasure to provide them with a solution that helped reduce their turn over rate and efficiencies.
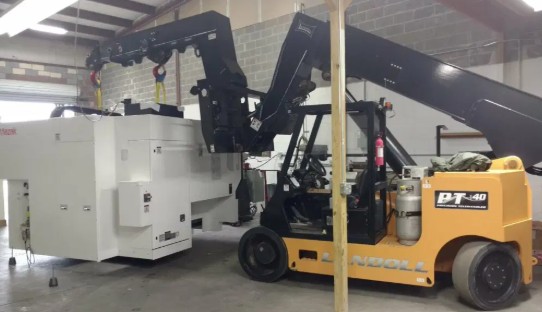
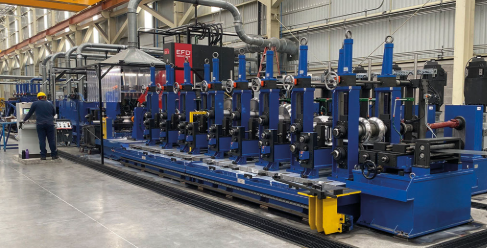
We had a client that stored large pieces of production equipment over years and they needed a clean out to regain the use of their square footage. We needed to find new homes for or dispose of: 2 CNC tubing benders, induction seam welding tube mill, small and large electric motors, caustic waste disposal, composites disposal and we handle the secure disposal of proprietary products and produced merchandise.
Product design, prototyping, & testing
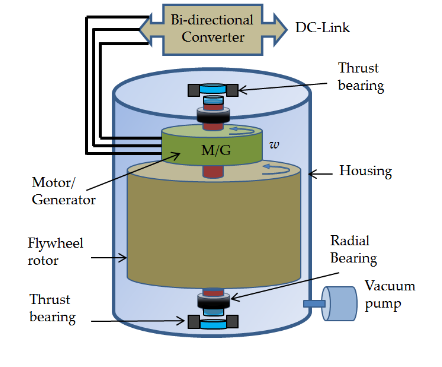
This is another one of those "we can't tell you exactly what we did" but here is what we can tell you. We had the pleasure to work with some of the best people and engineers at Torus. We and worked collaboratively while creating competing designs for the soon to be in production bearing system in the FESS (Flywheel energy storage system). We had great success running the prototype system that was built. It was designed around information and data from prior testing. We have the hope that one day torus will put "our unit" in a museum along side the other major stepping stones representing torus's path to success in changing the energy industry forever.
Disclaimer: What is illustrated above is just a basic understanding of what a FESS system is. It is simply a visual aid with the intent to help those who have never heard of a system like it understand what it even is. It does not reflect what the teams landed on as the viable solution, nor does it reflect in any way what exactly was tested, or why/how.
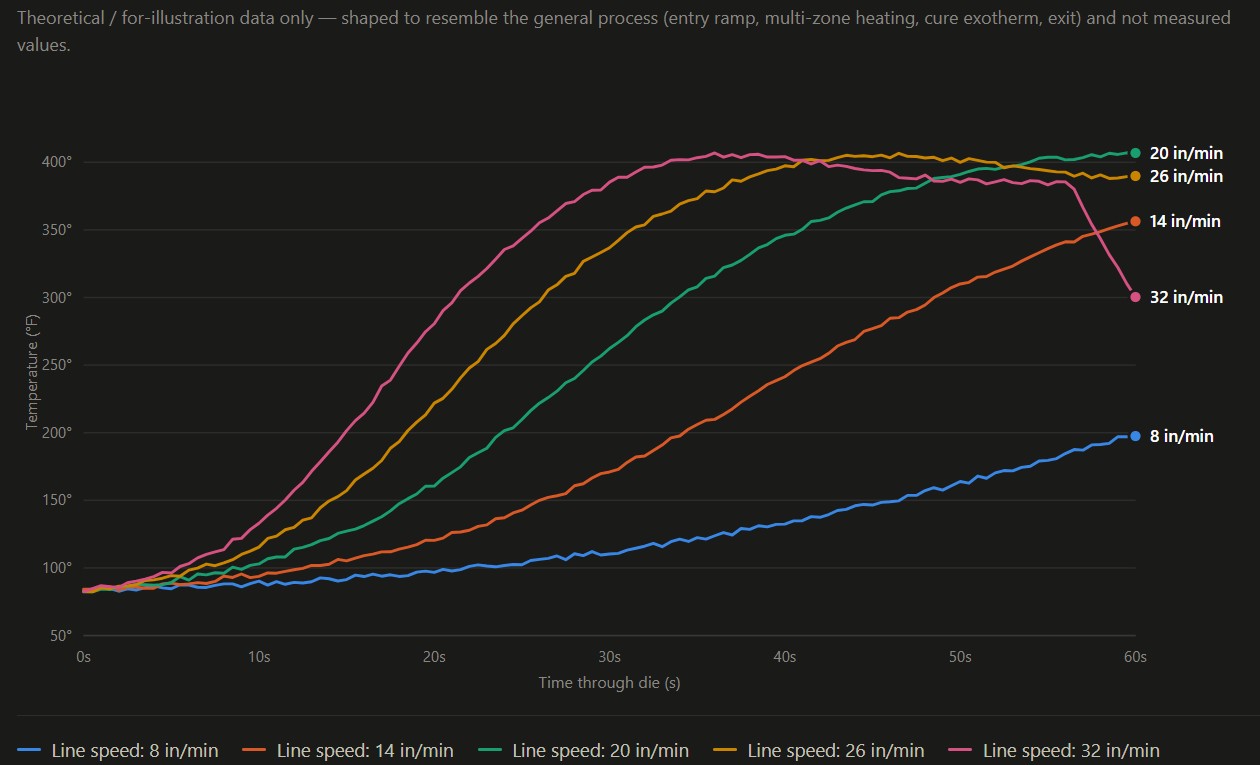
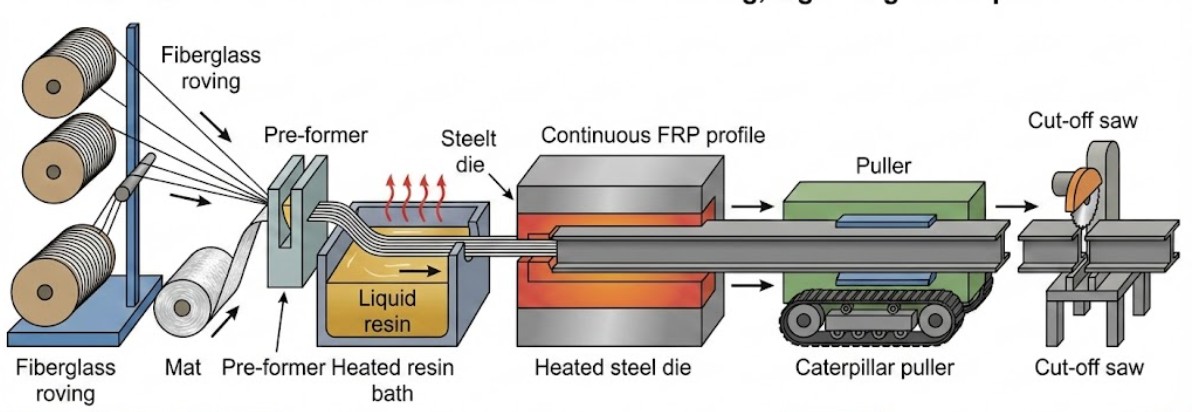
We studied Easton's range of tent and archery products by threading a sacrificial thermocouple wire down multiple dies as the production line ran in order to establish temperature curves of the cure process. Through doing this we were able to determine at what location the resin is completely cured and thus completed the exothermic thermoset process. With the new found knowledge we were able to increase the line speeds across all products. We discovered you could run 25-30% faster and still get a full cure while on the most temperamental products we were still able to achieve a 5% line speed increase. All products were tested for straightness, concentricity, appearance, then tested to failure under multiple load scenarios ensuring the end product was high quality as ever.
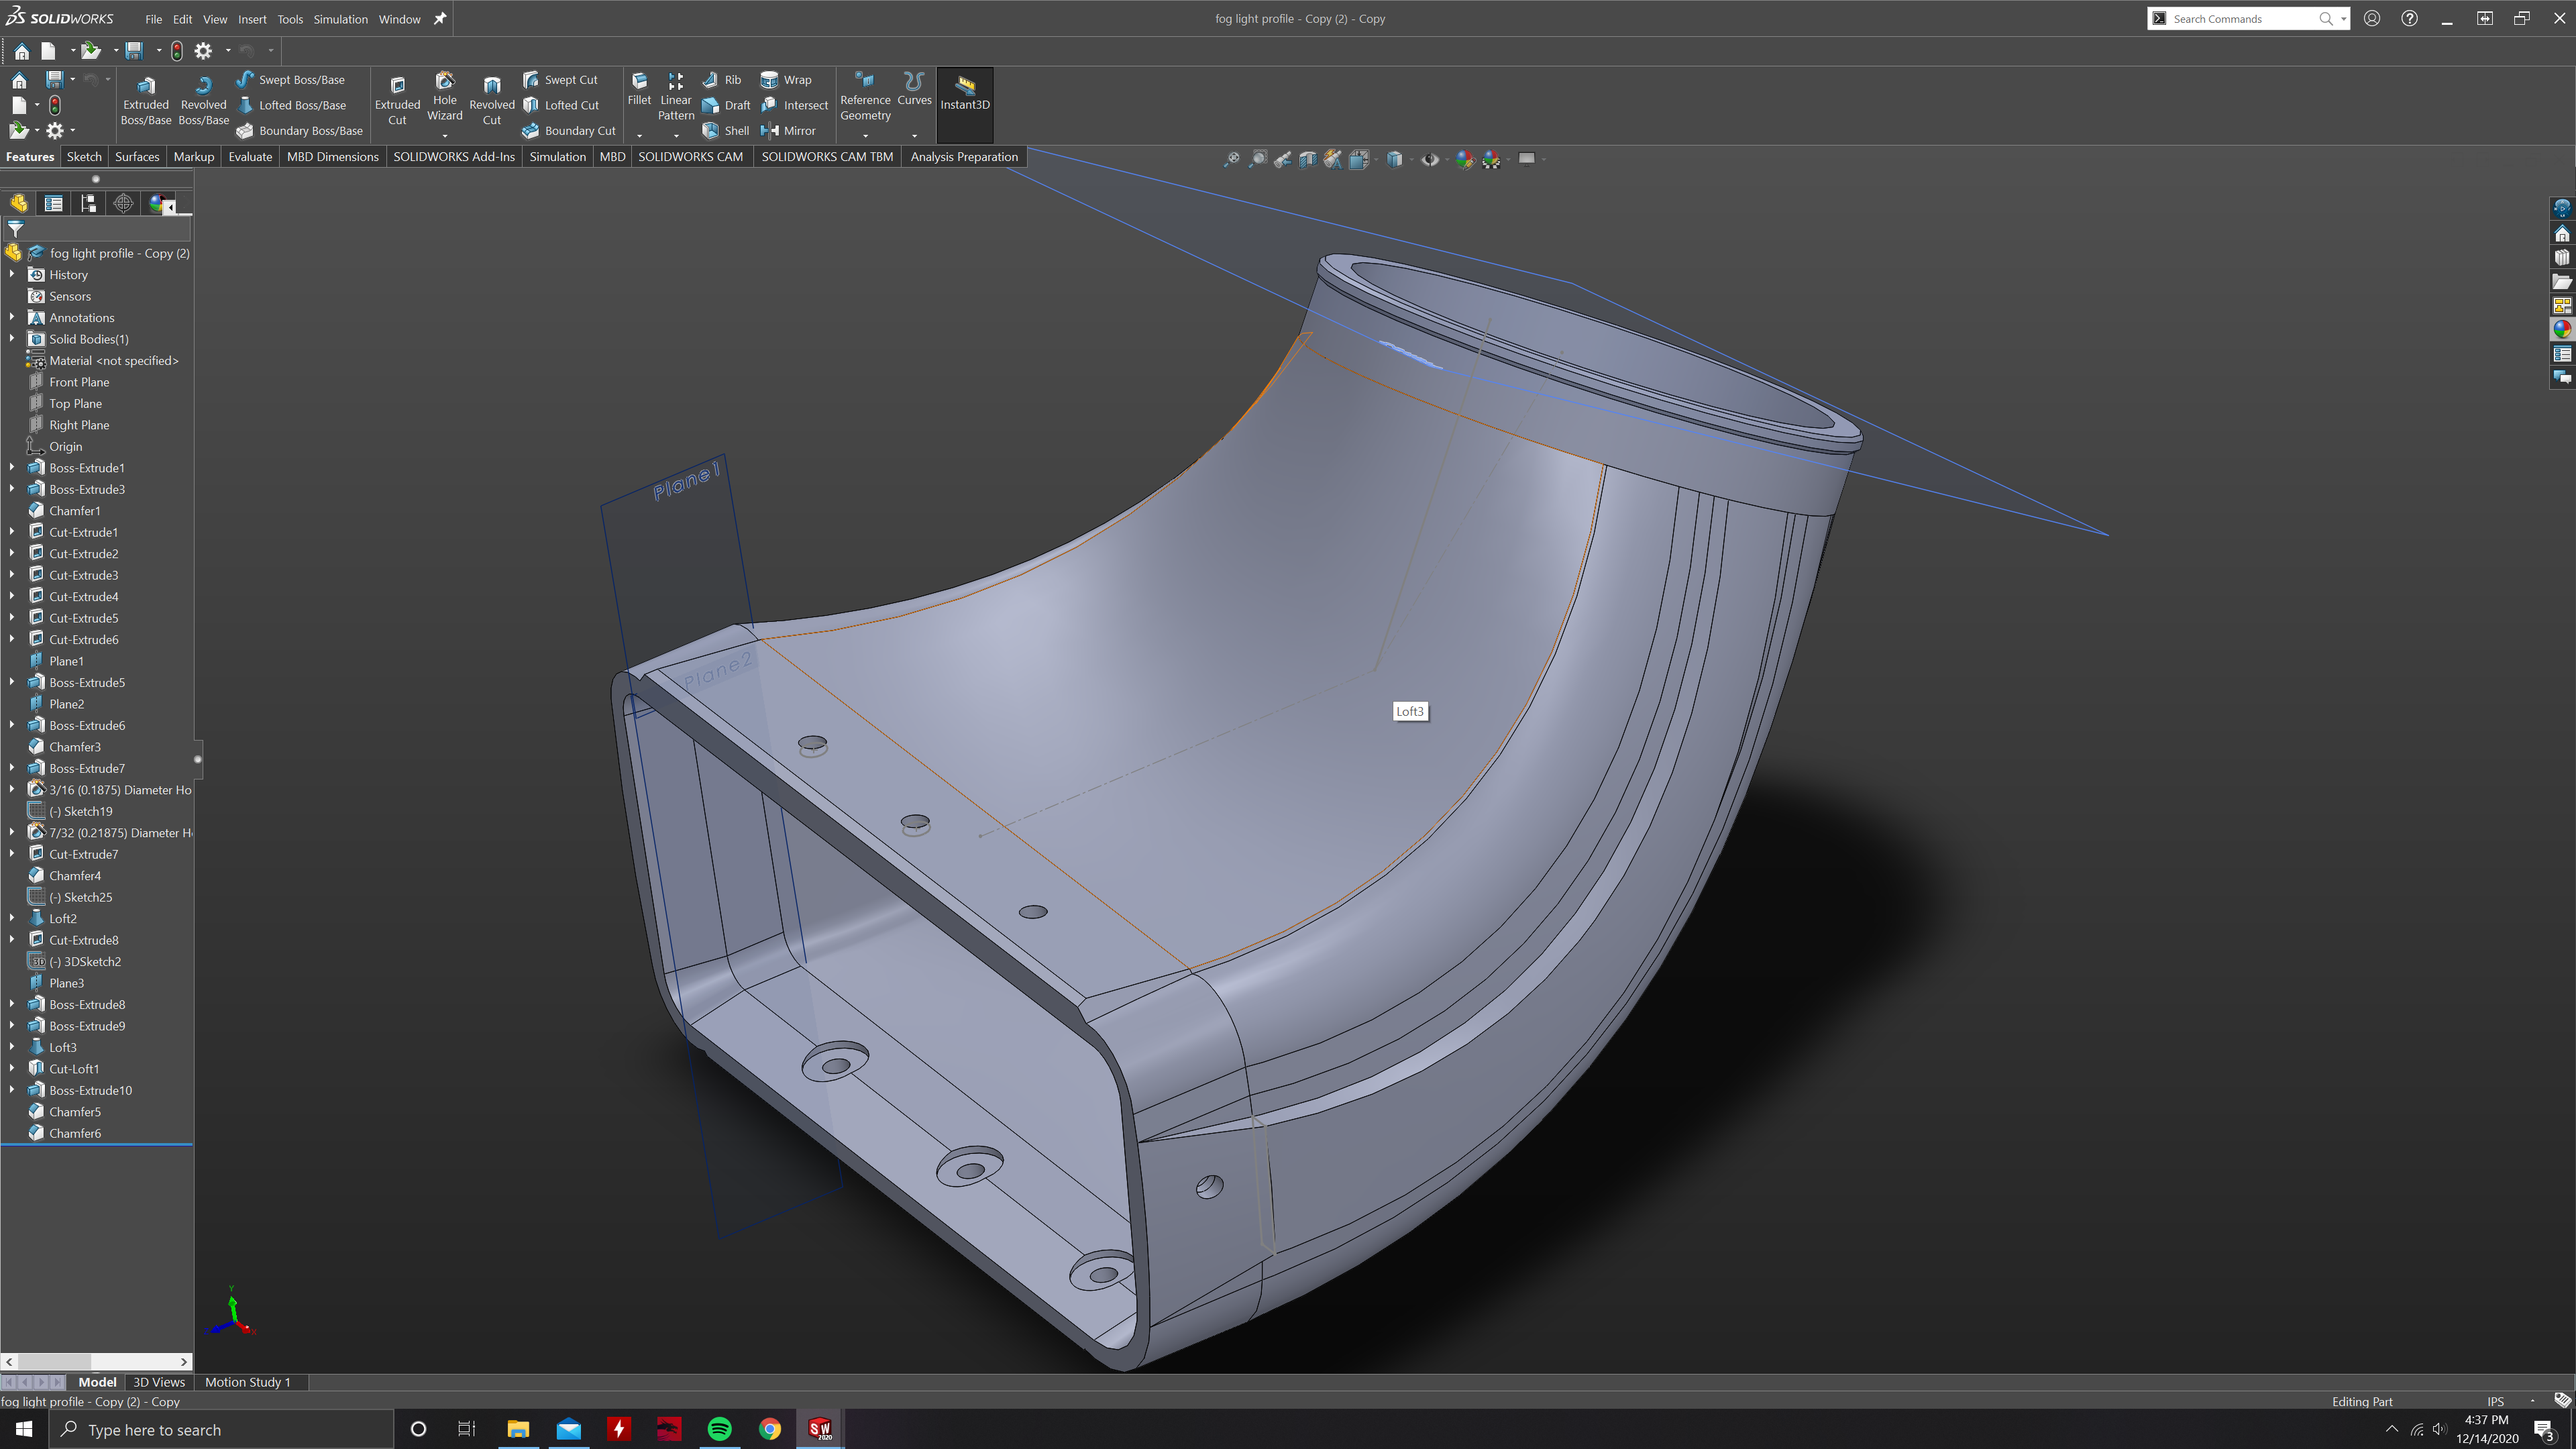
 photo
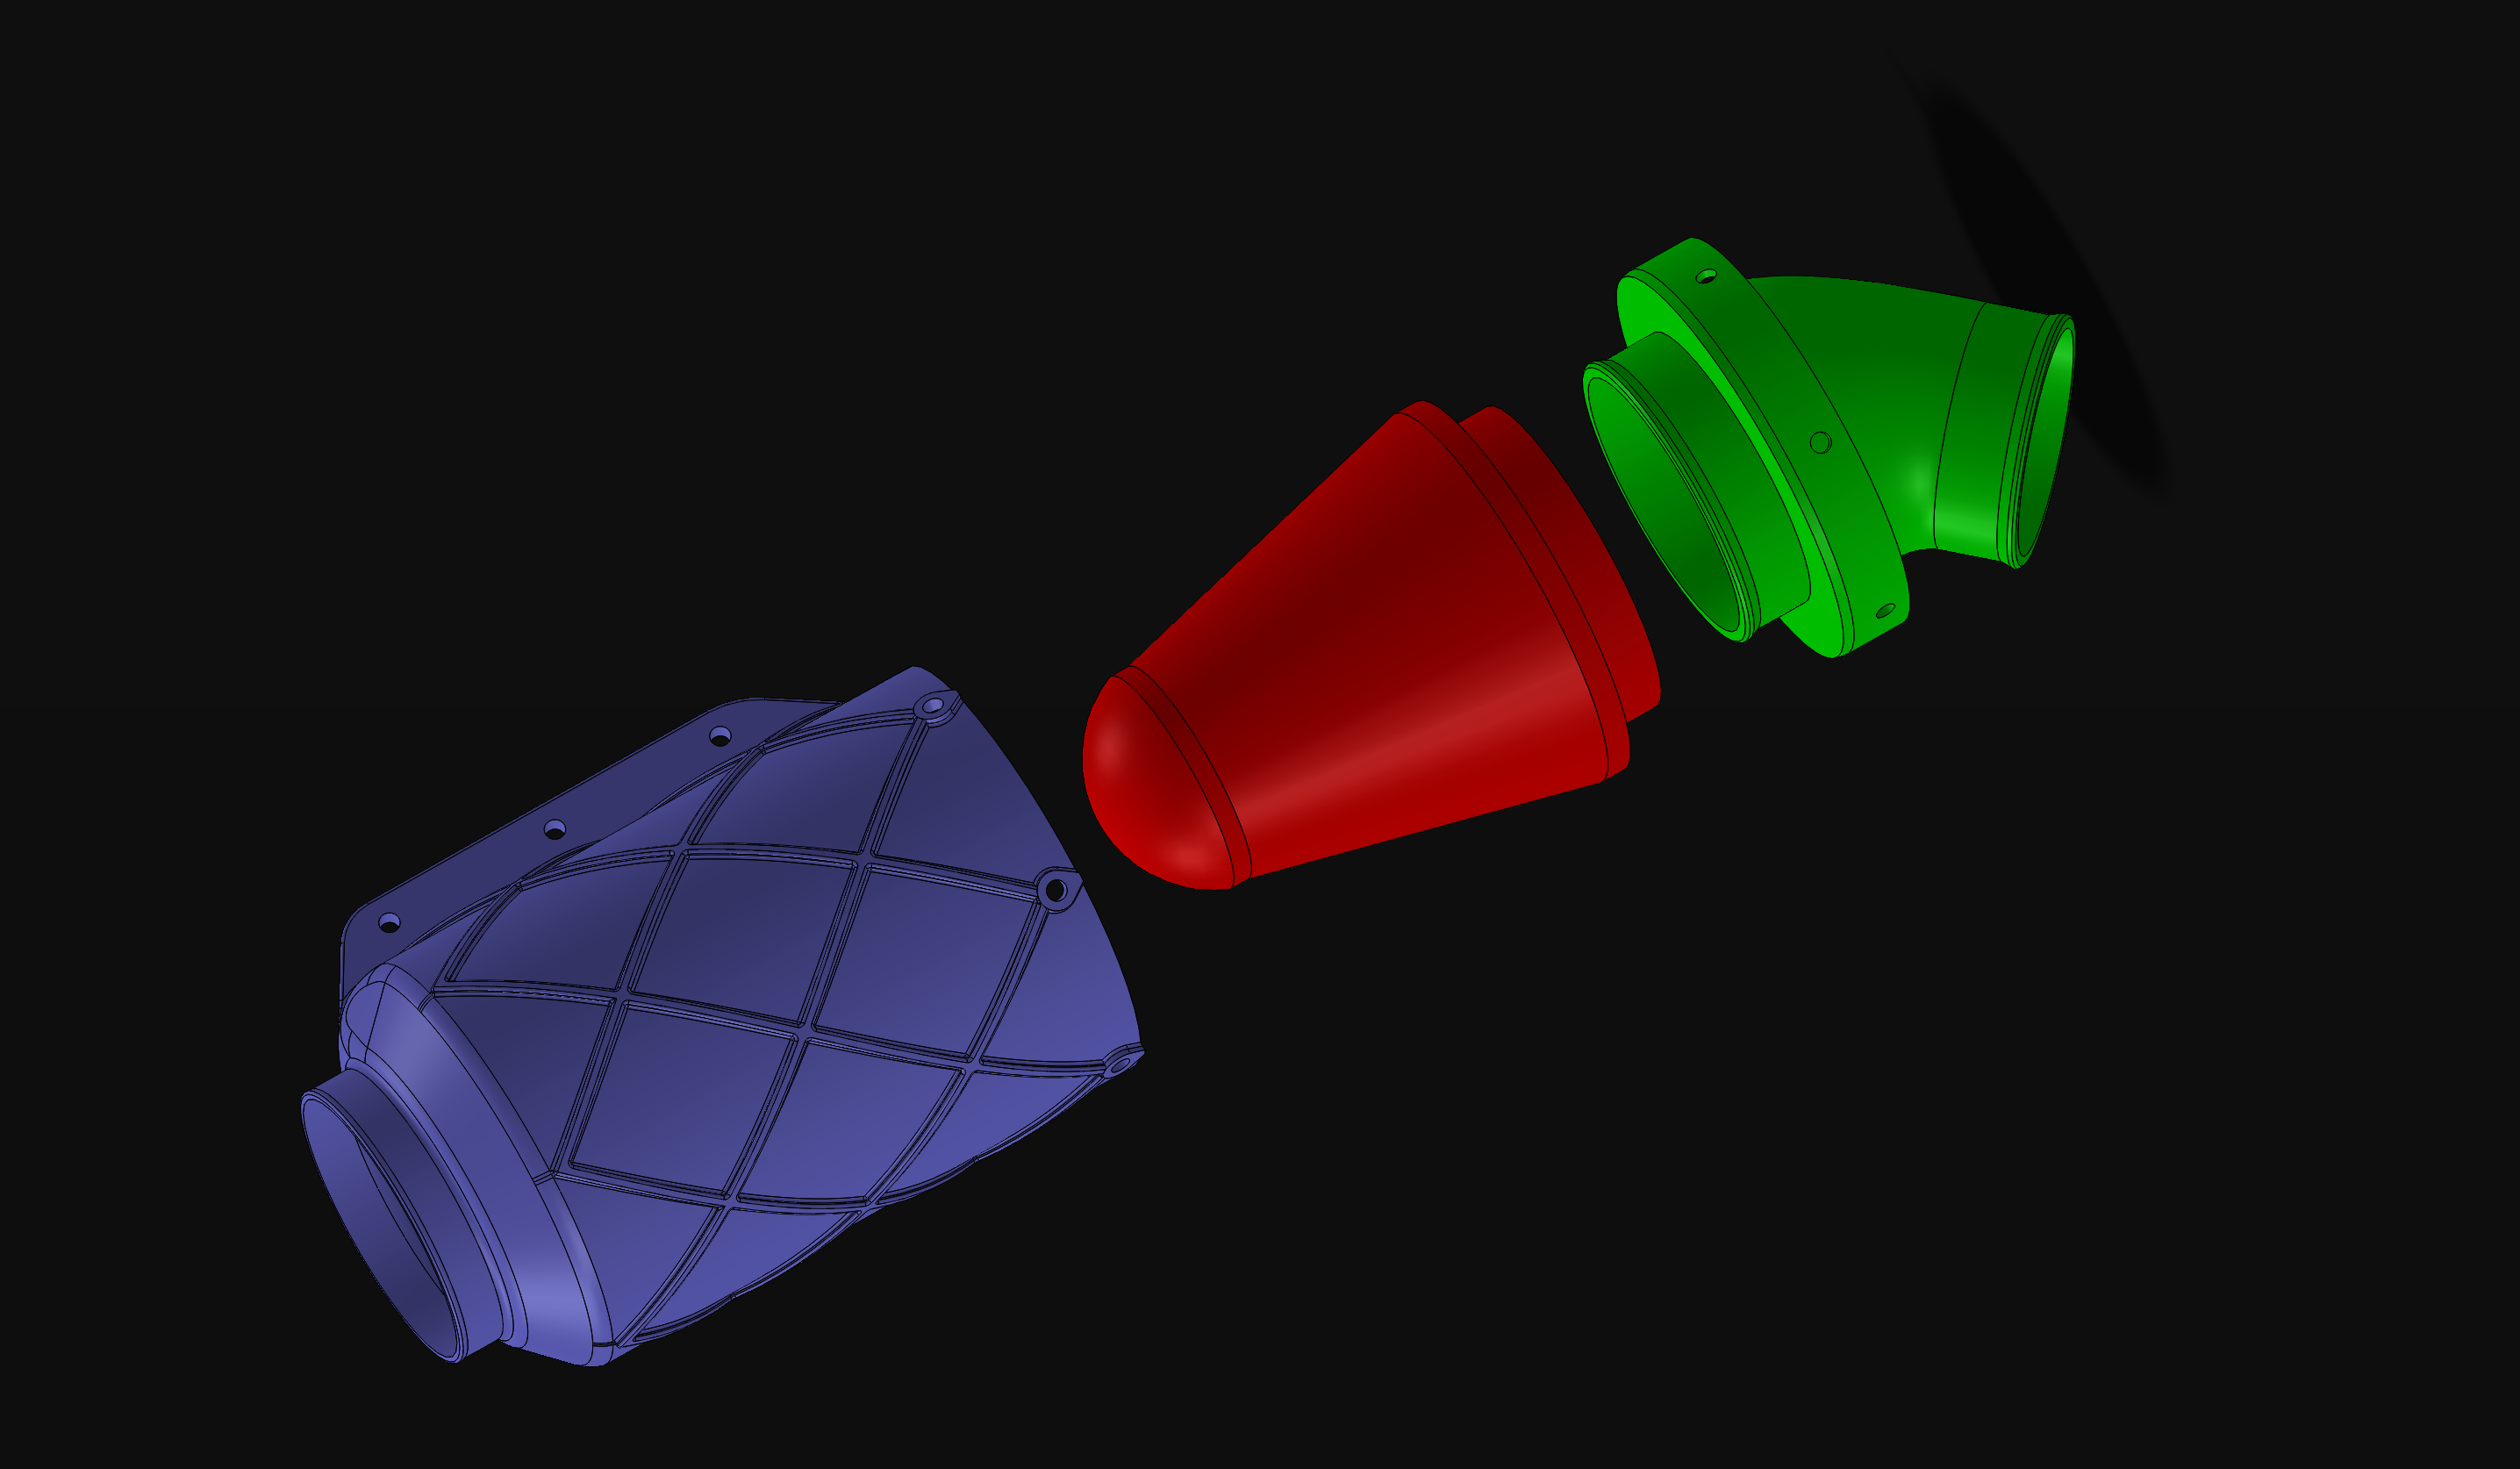
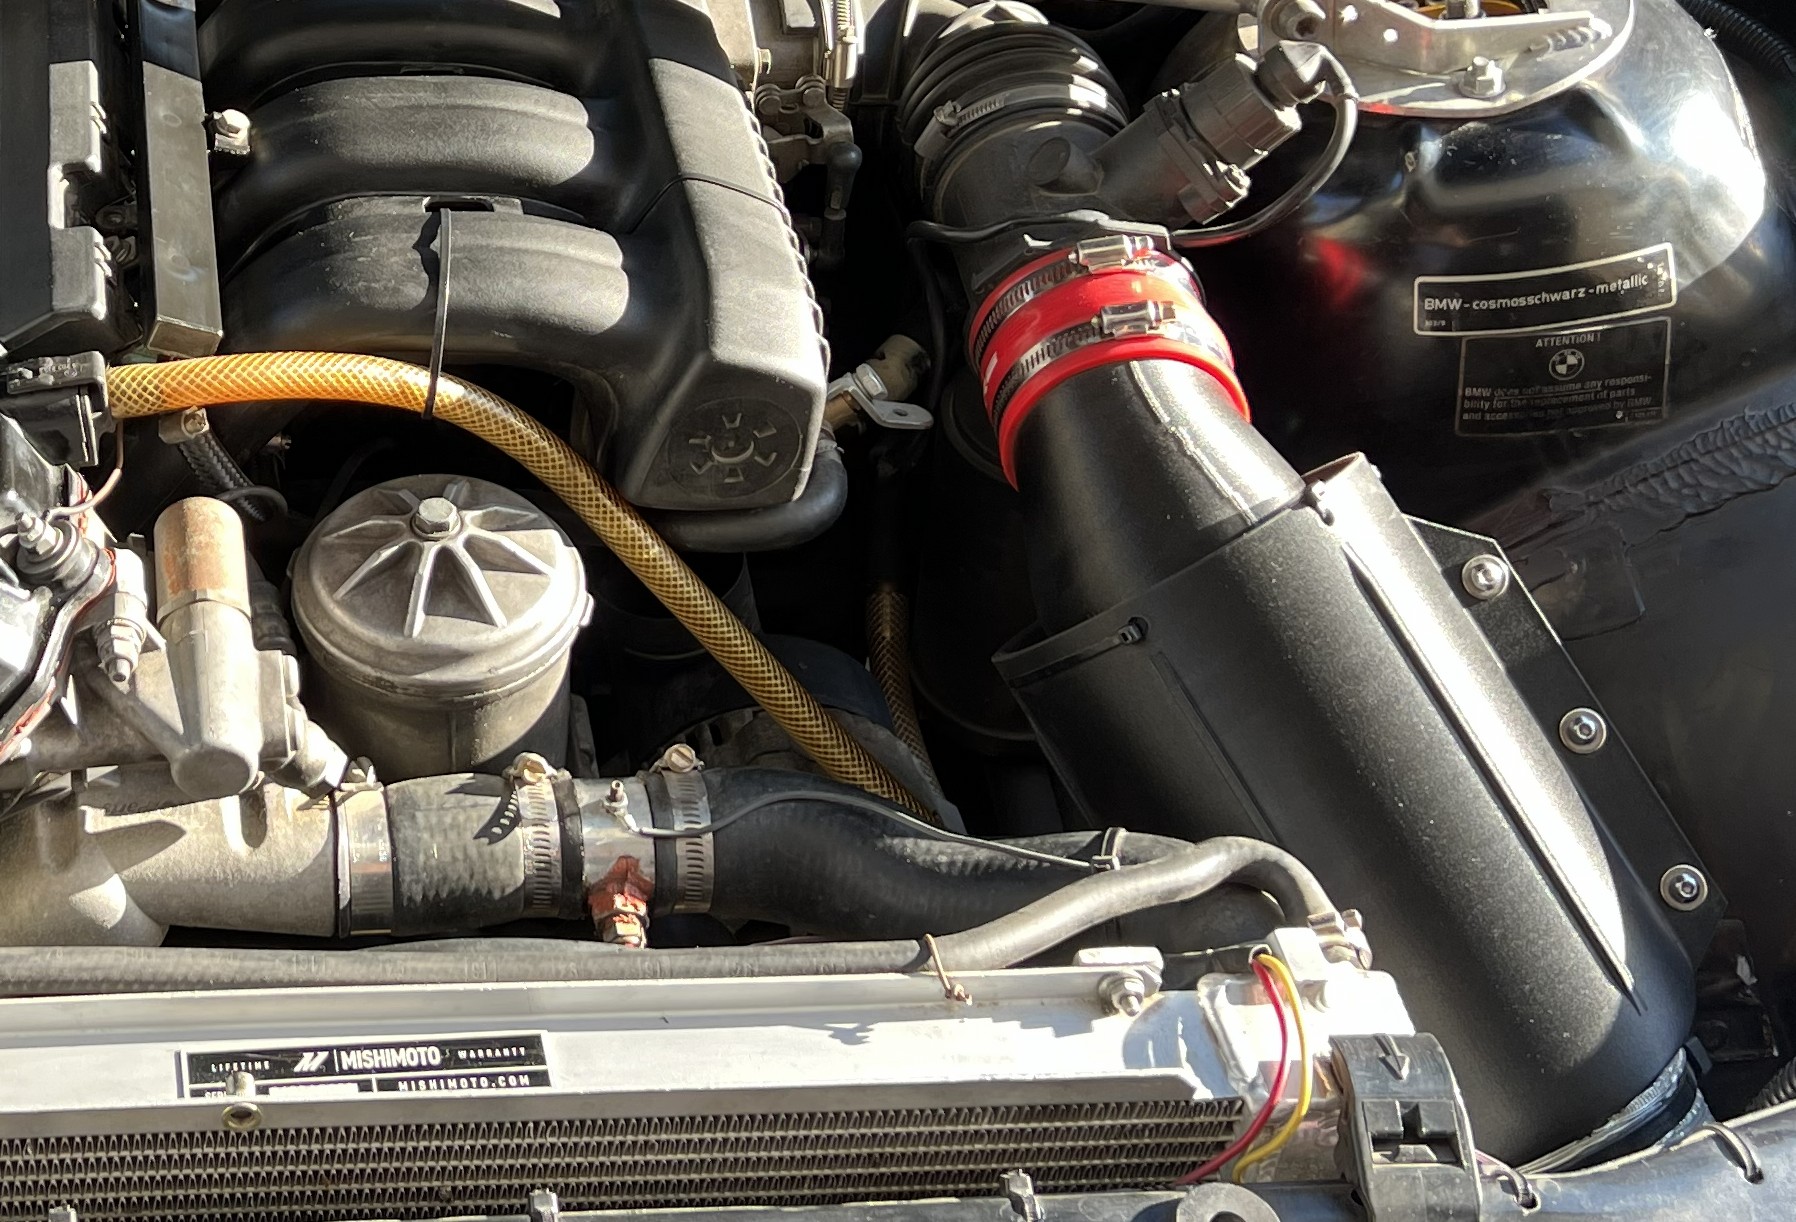
Ground up design focused around building a retail level product that can be sold with confidence and perform in variable conditions while being easy to manufacture with a printer. The system was flow tested using airshaper, was printed out of common CF-nylon, and ran in a e36-M3 BMW (street and track use case) for 5+ years with no signs of cracking or deformation over time. We are better than anyone else in the business when weighing attributes vs necessities during the R&D process to get you the best real world solution to your problems.
Fabrication & fixture design
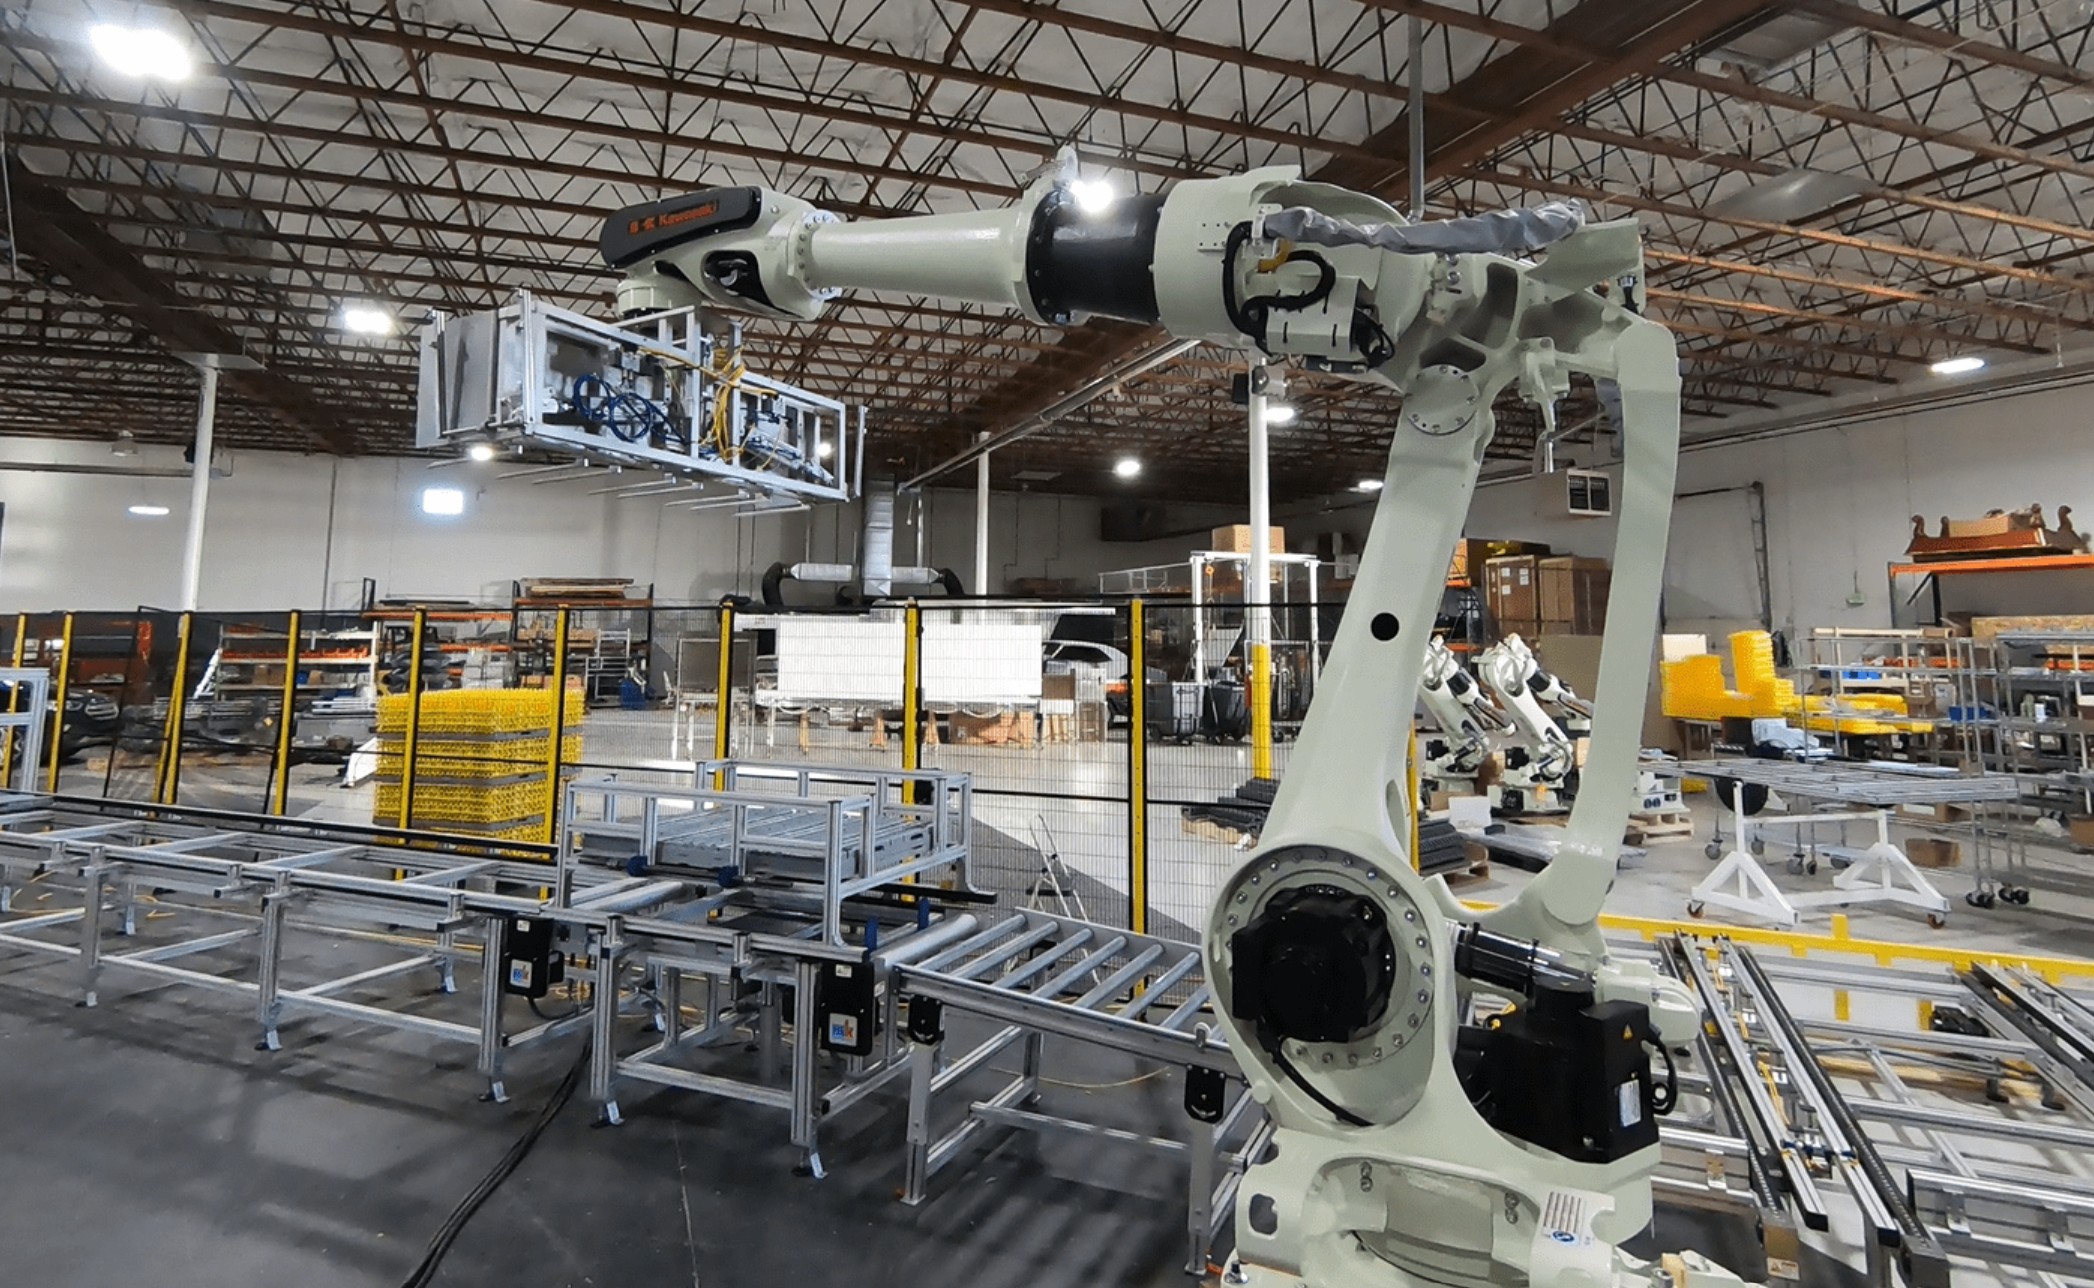
Picture this system like a multi-fork forklift, on a robot arm. Each set of forks picks up a Costco-sized container of eggs. 4 simultaneously in a row, that's why it is 4 feet wide and stacks them on a single pallet. One row at a time. For this project we were given basic drawings with only nominal dimensions for the aluminum end effector frame. We then had a quick conversation with the client to gain more context regarding the loads and application. From that point MyEngineer handled the rest. This worked out well as we used 1"x1"x1/8" wall square aluminum tube for the frame to keep it light and easy to clean/maintain.
Note: We design and fab robot pedestals/bases of all heights and load requirements fit to your needs.
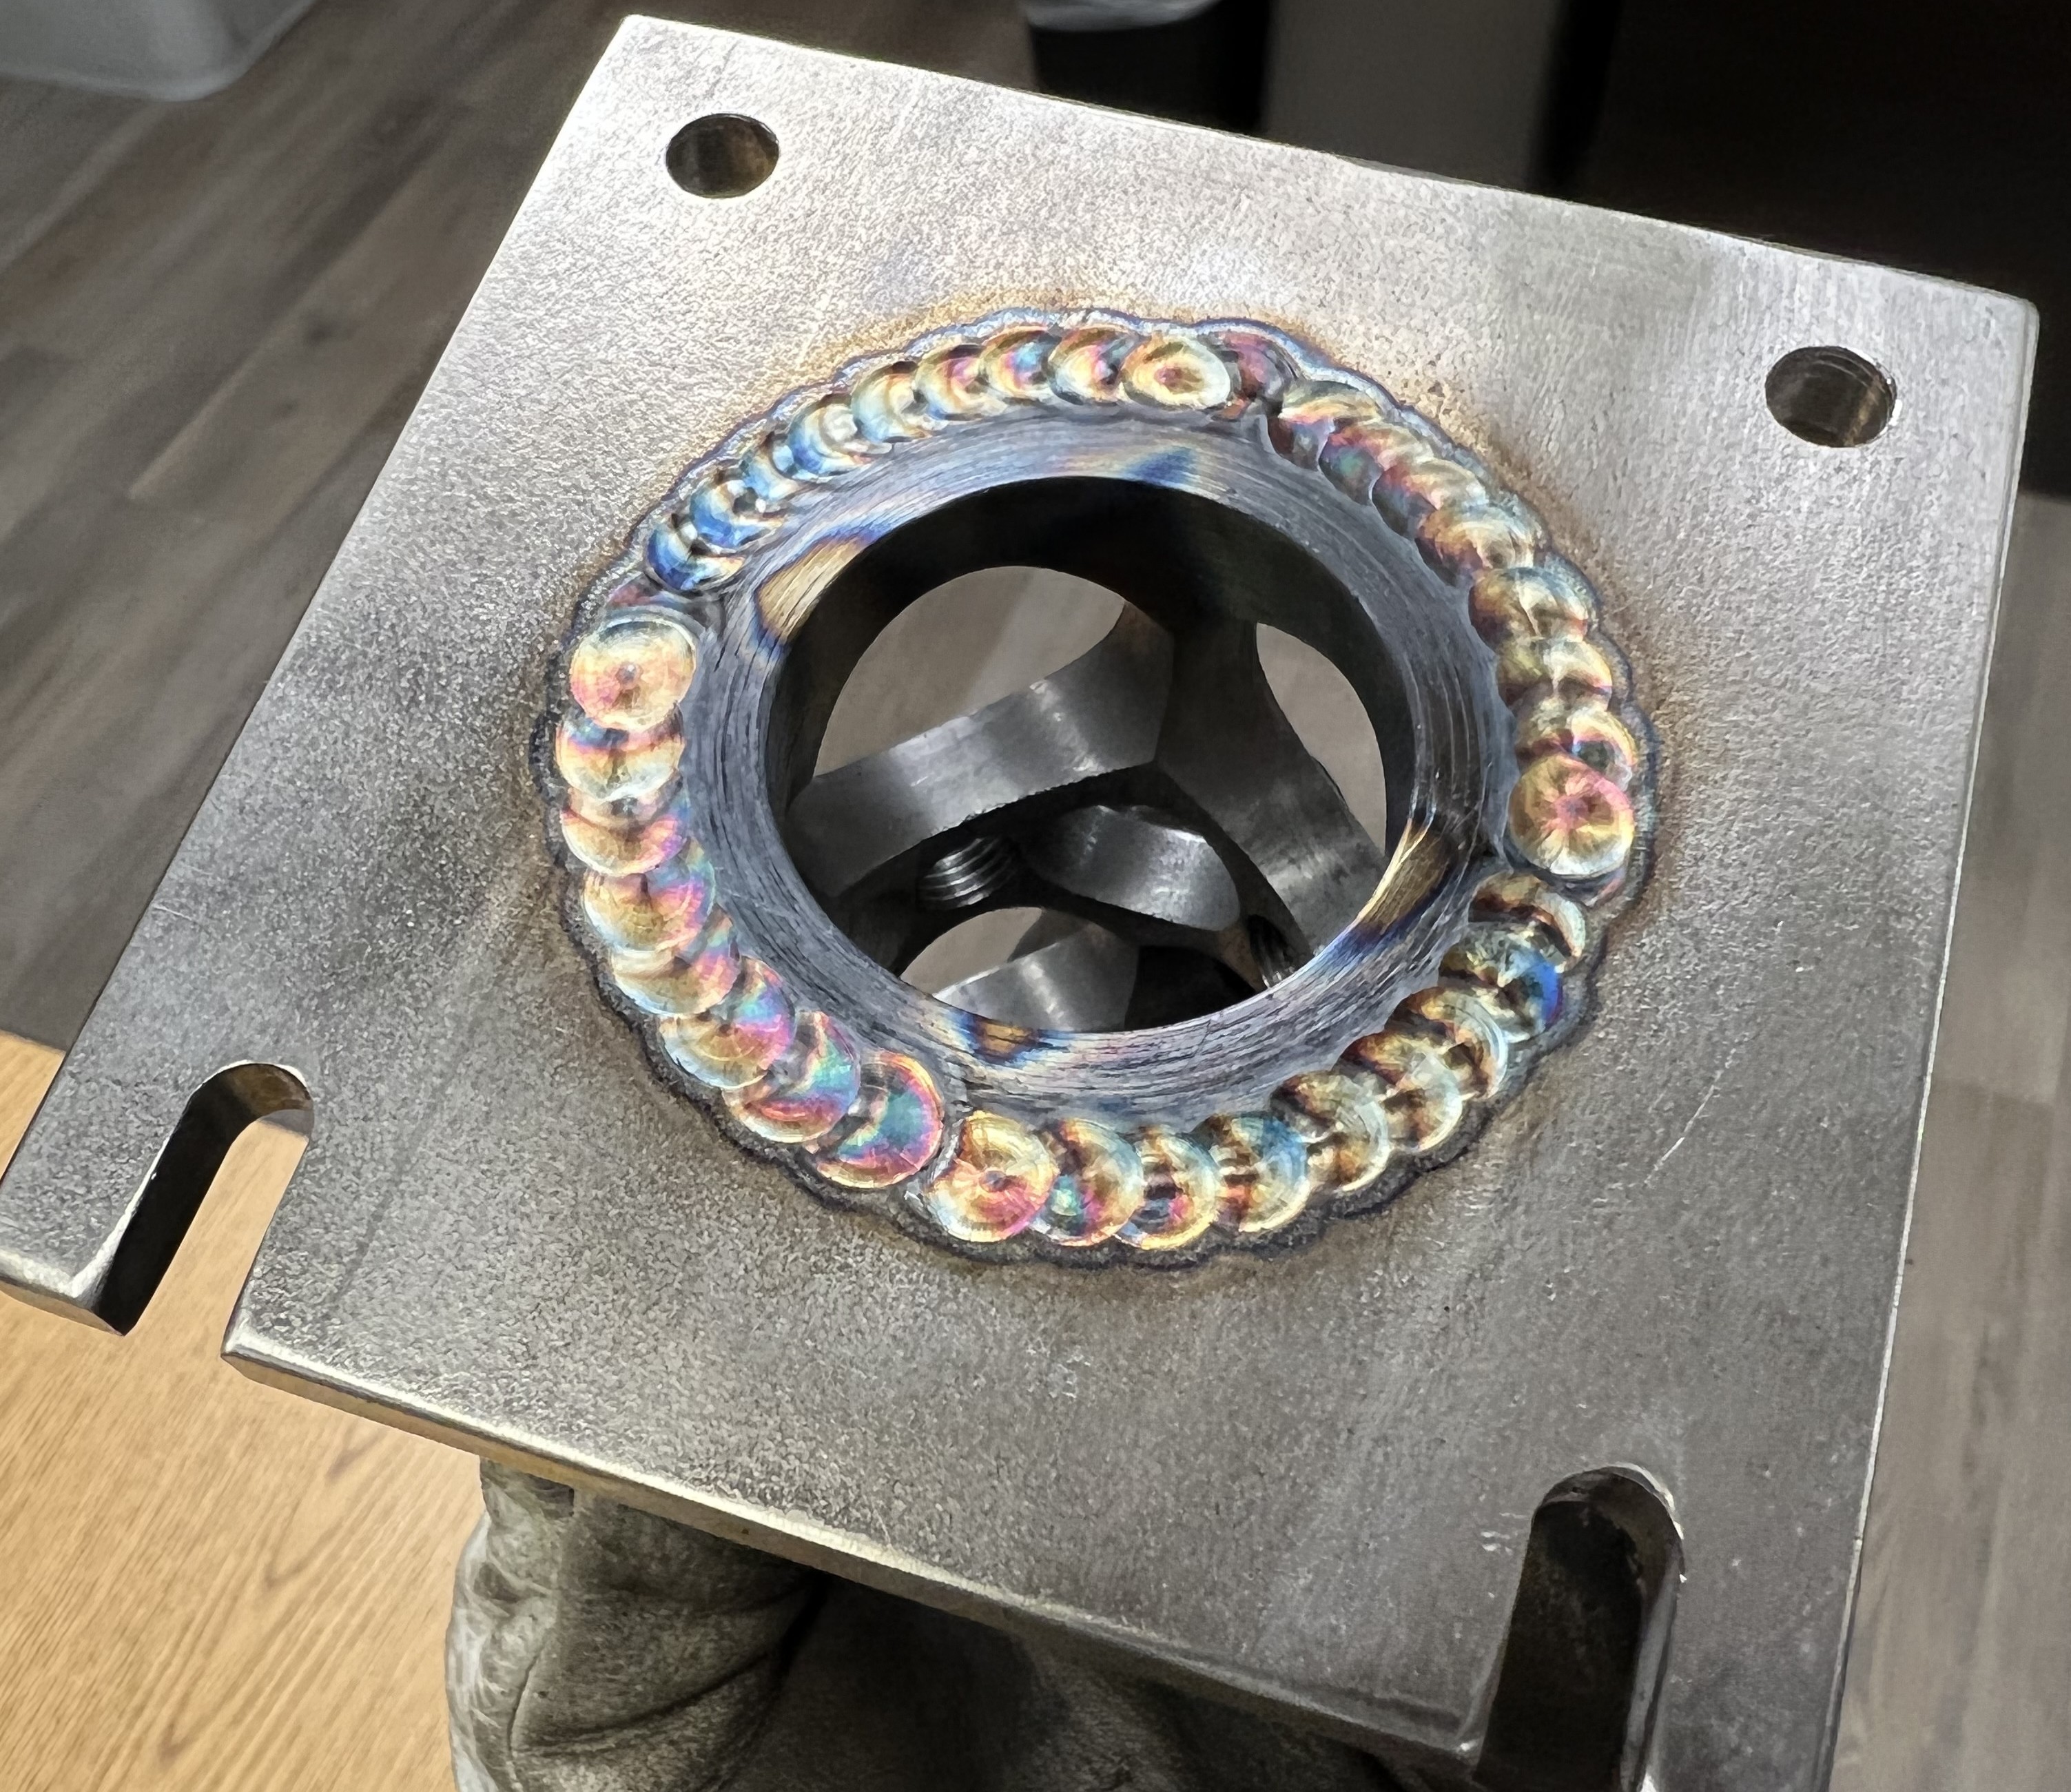
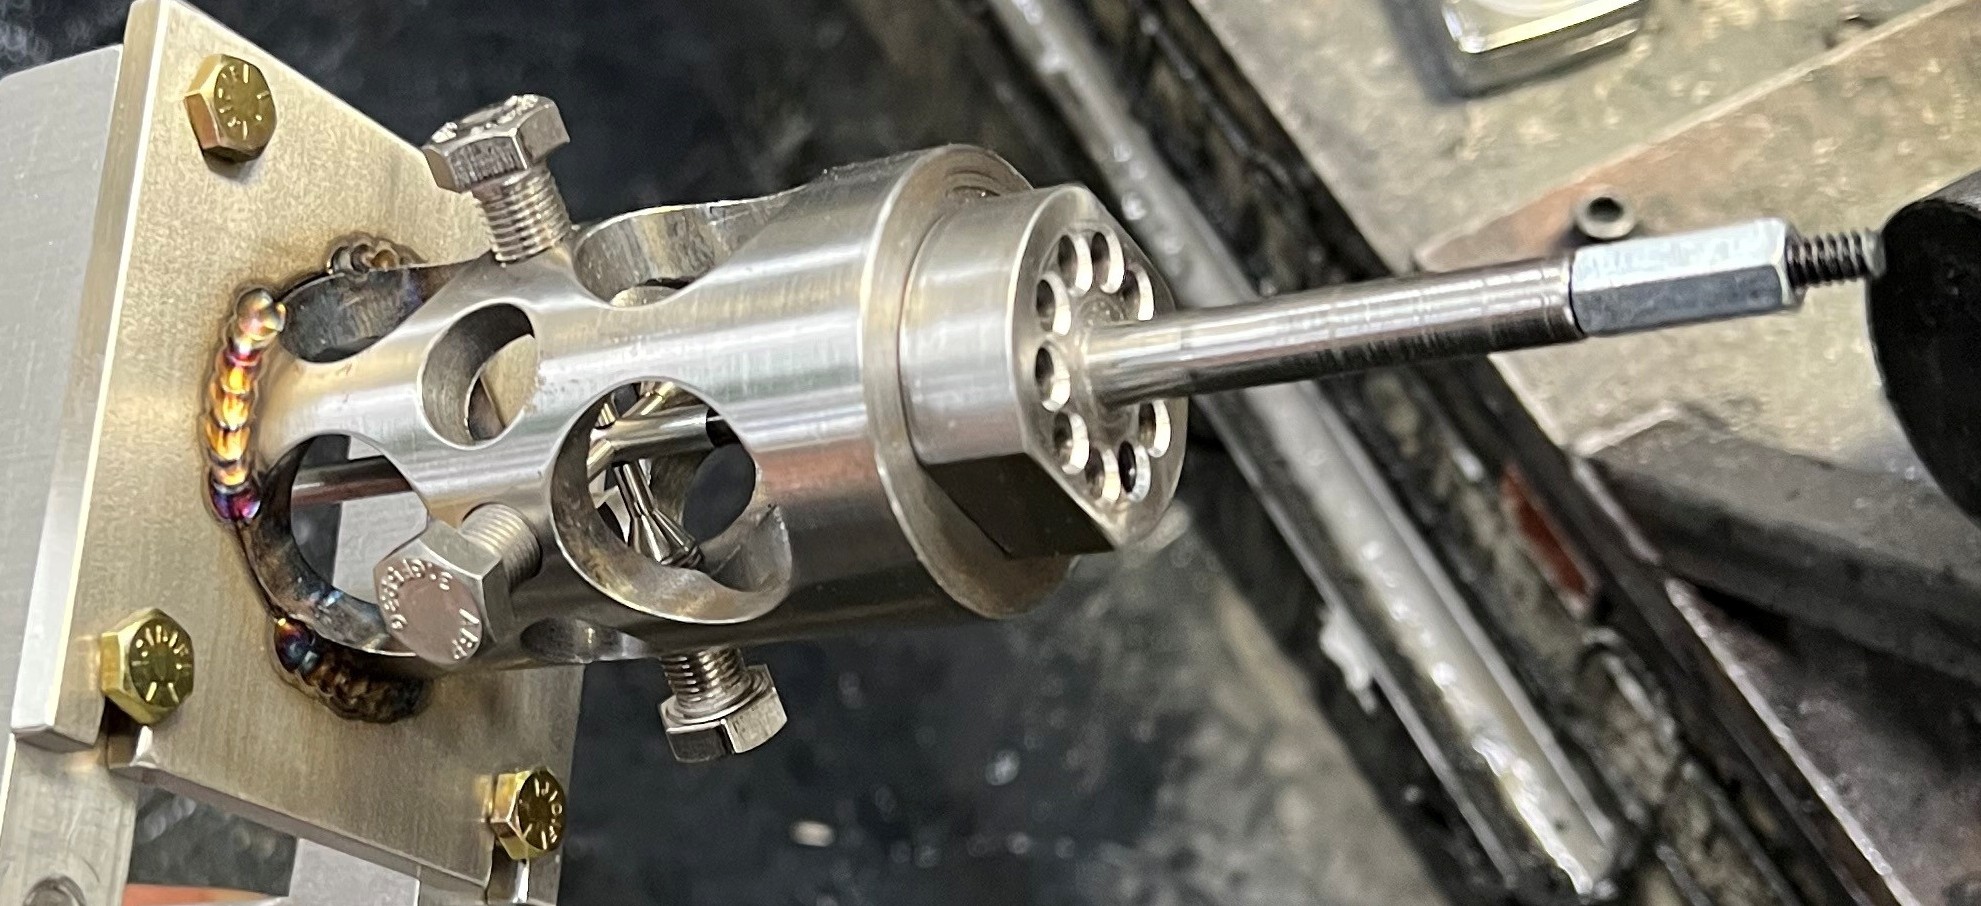
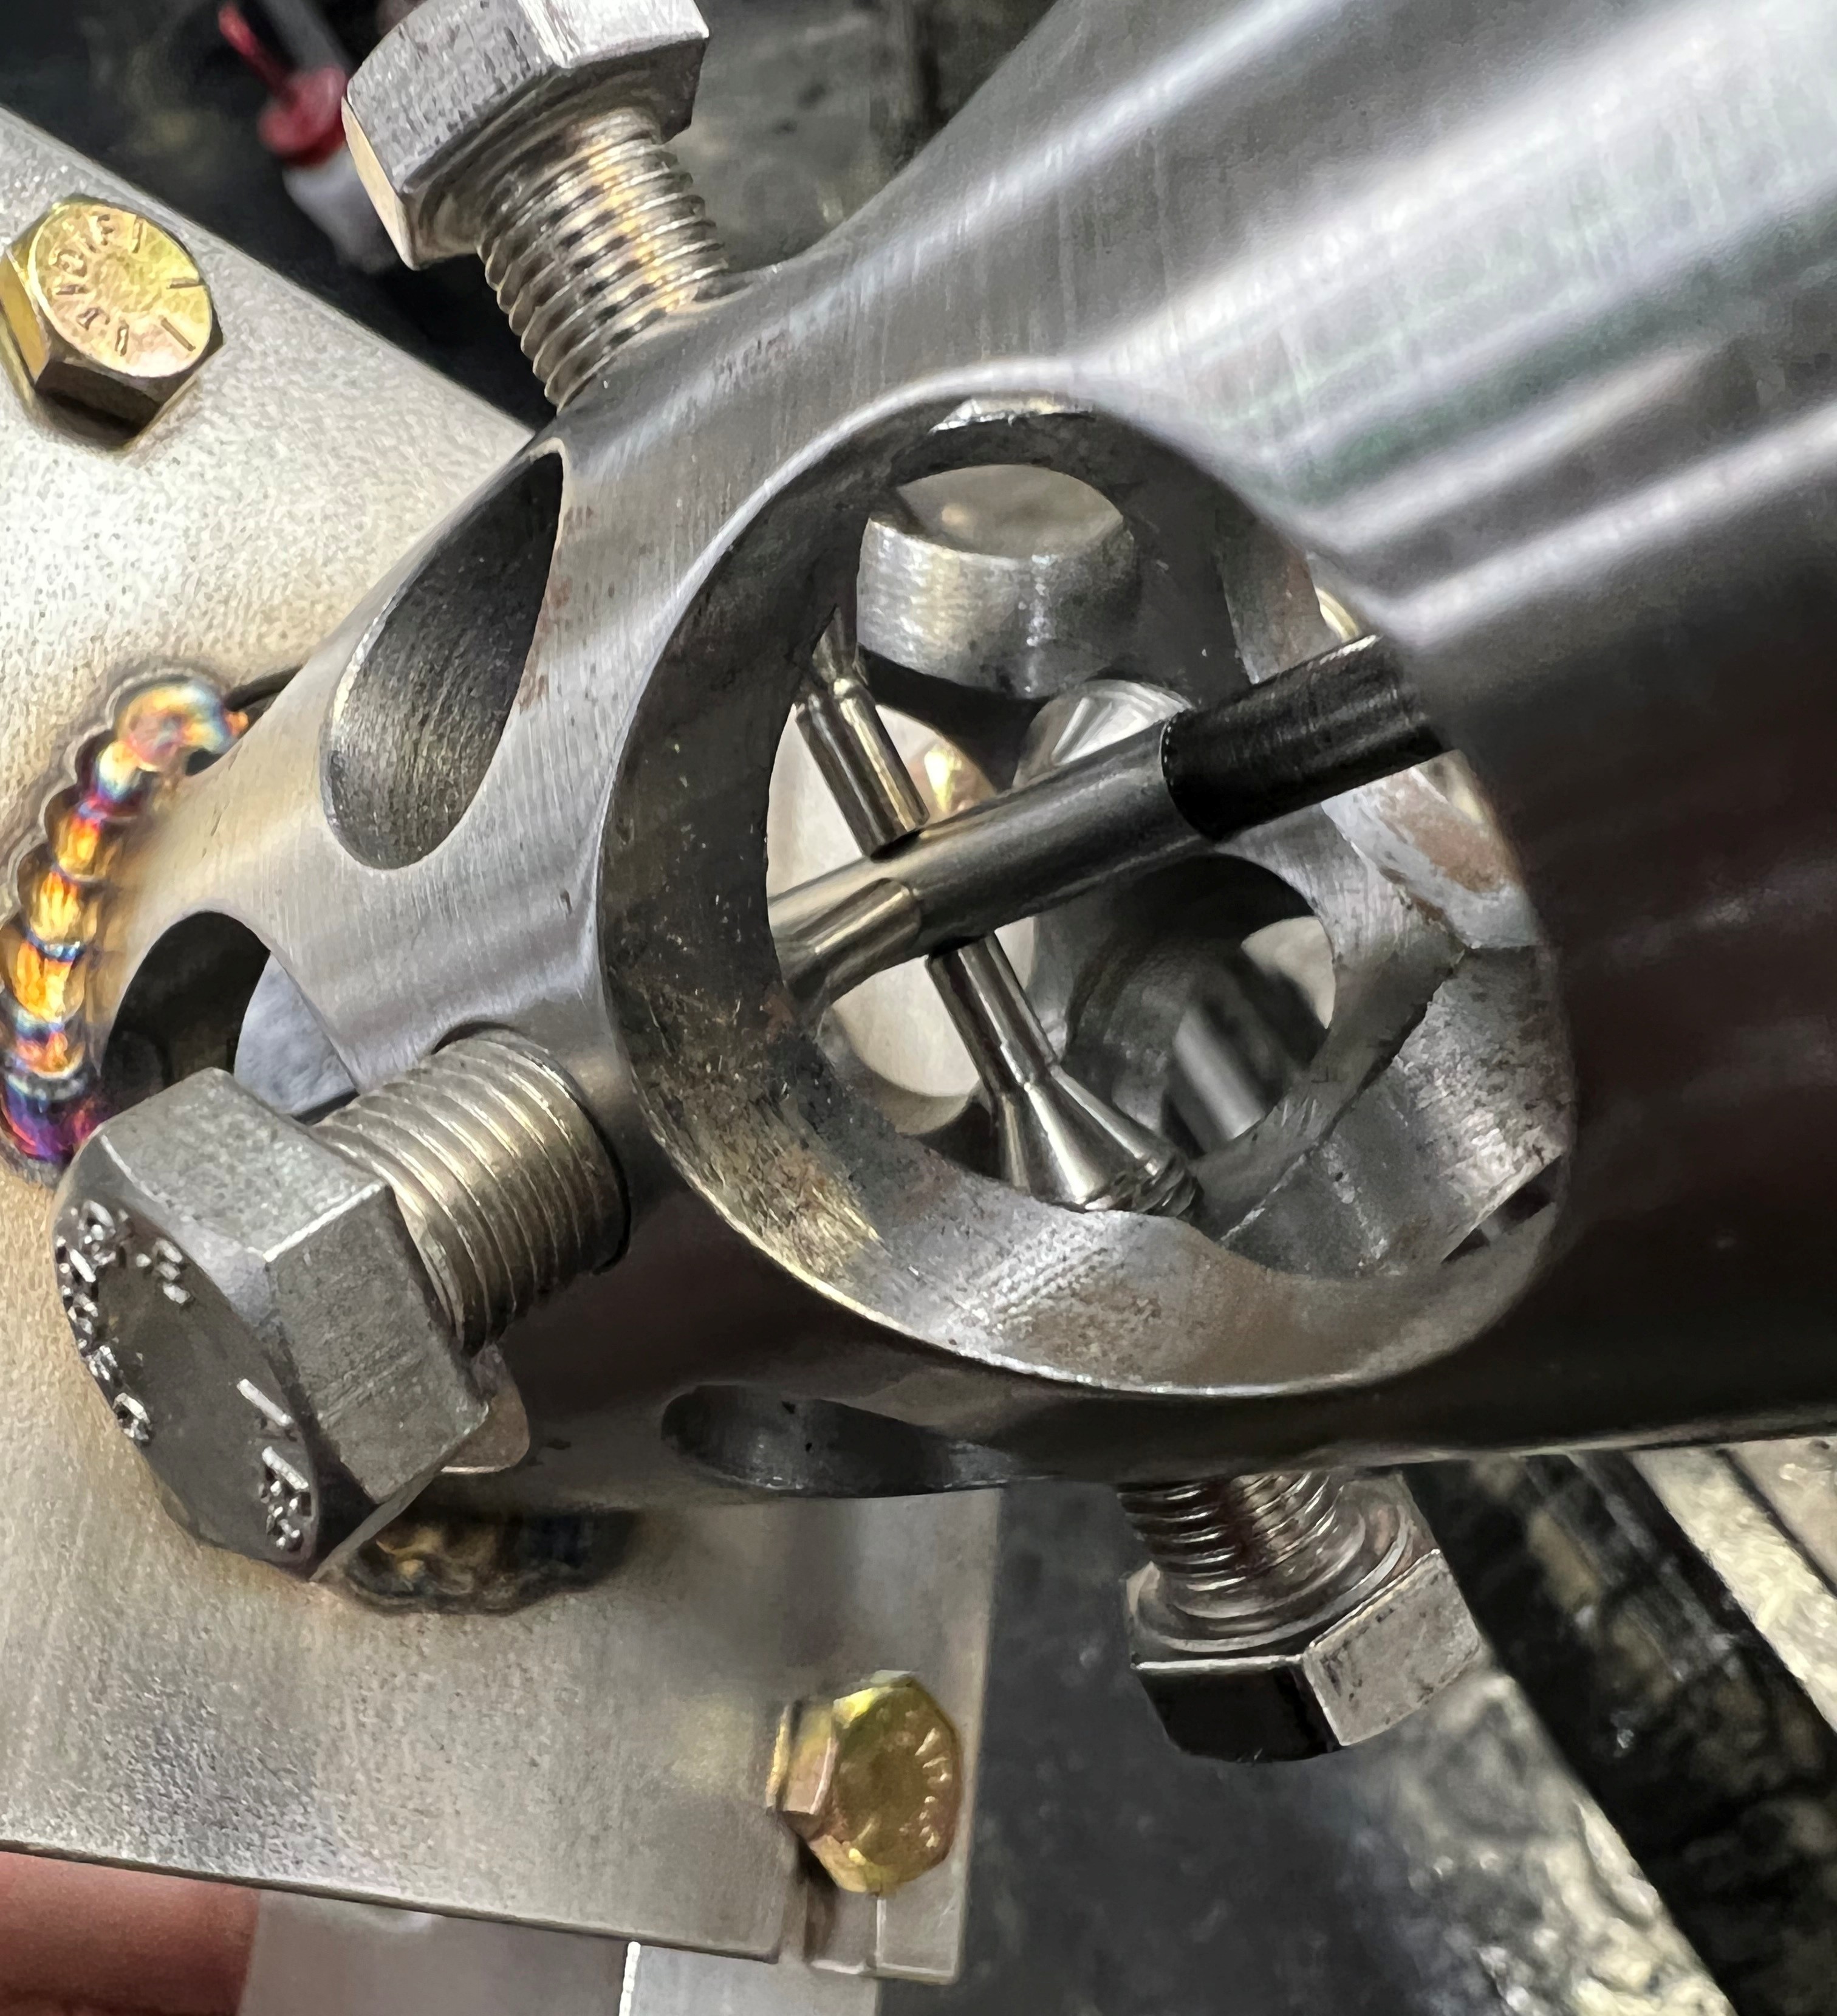
We can tell you we designed it based on reverse engineering an original component. The goal was to greatly reduce the cost to manufacture this component while working with production feedback to design something overall easier to use at the same time. This was a great success and it was a pleasure to work with those on the production floor to improve ergonomics and user friendliness of the device.
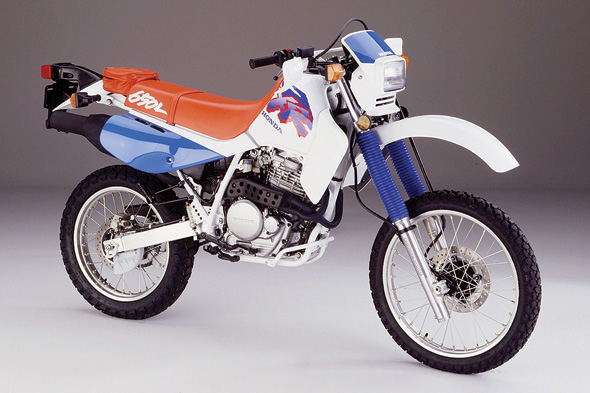
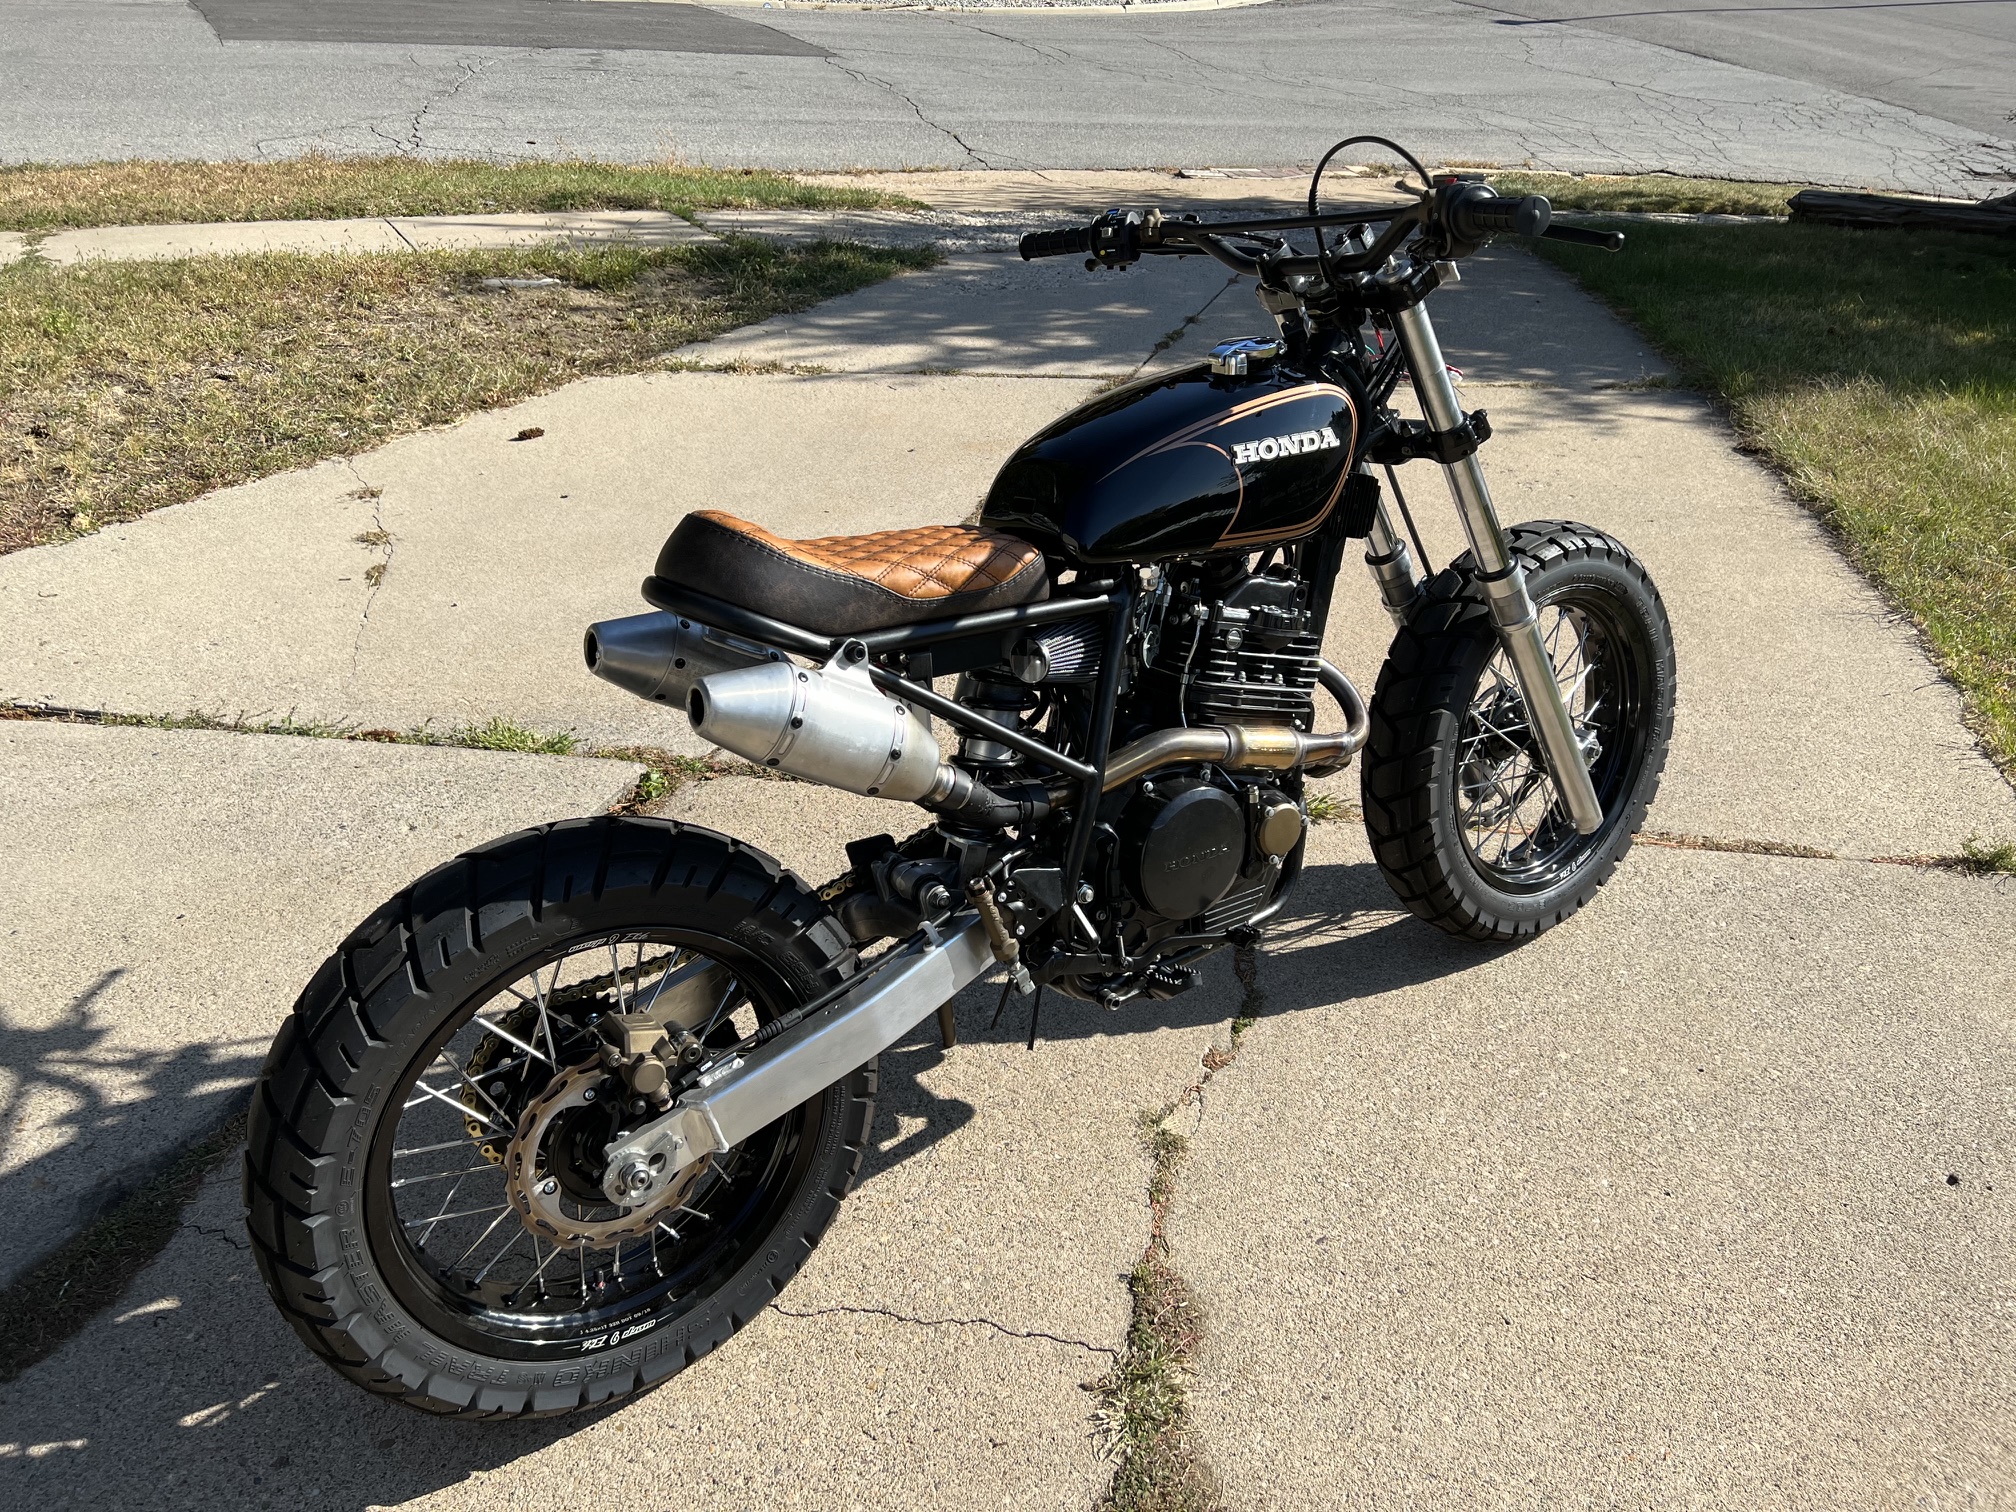
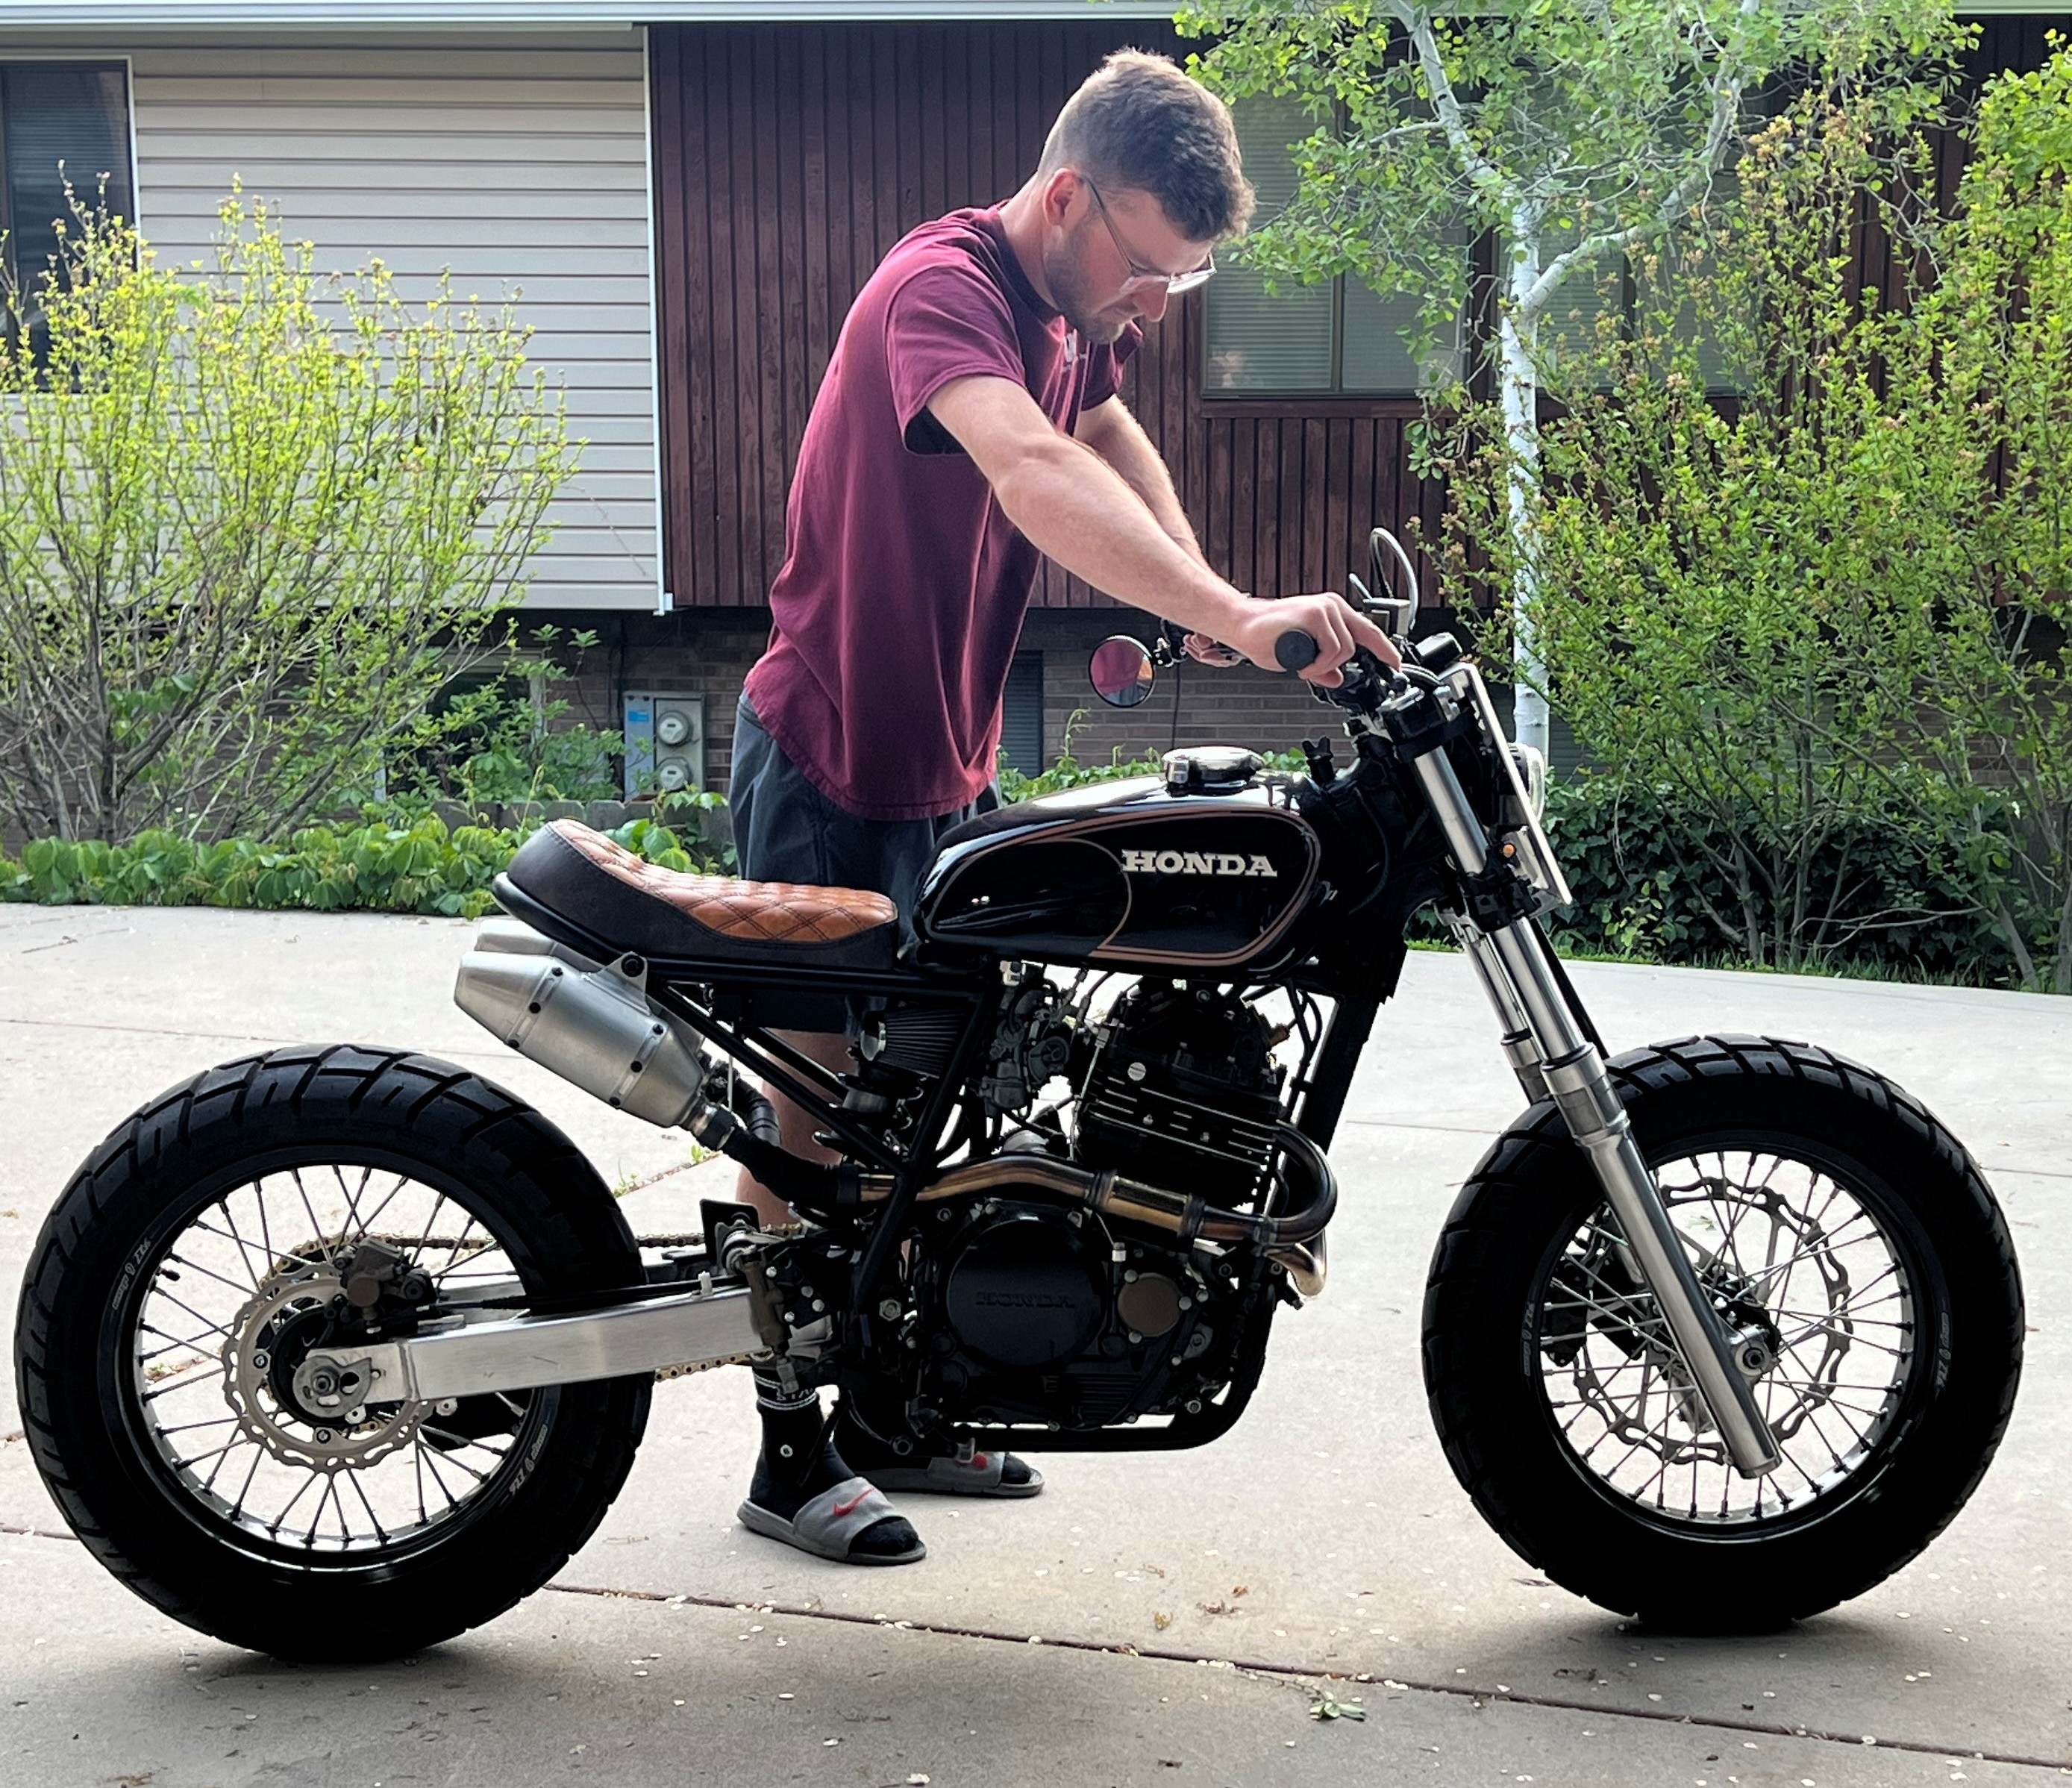
This is simply a demonstration of how diverse MyEngineer's fabrication skills are when tied to a fit and finish project.
This started life as a Honda 1999 XR650. Every tube, engine cover, engine case, hose, headlight/number plate has been cut, shortened, welded, 3D printed, machined, rewired etc.
Large format, advanced material 3d printing
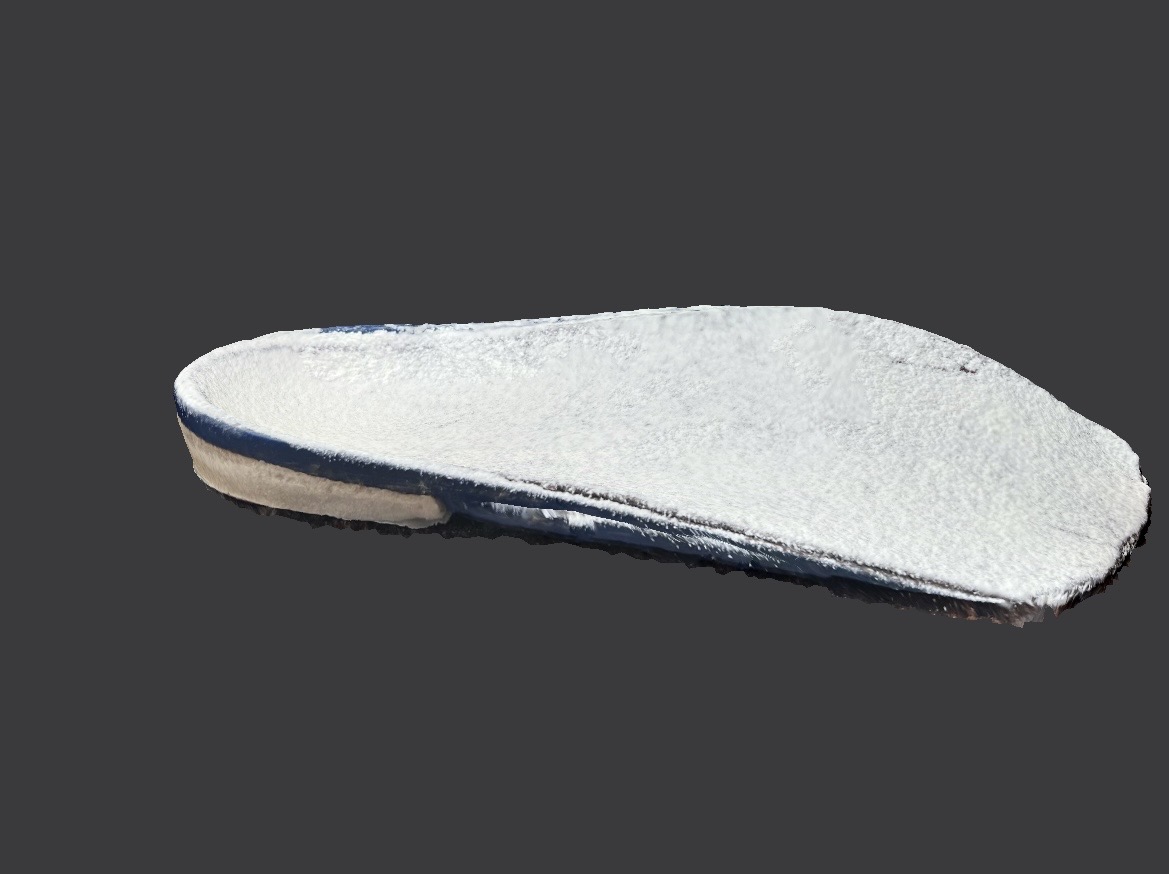
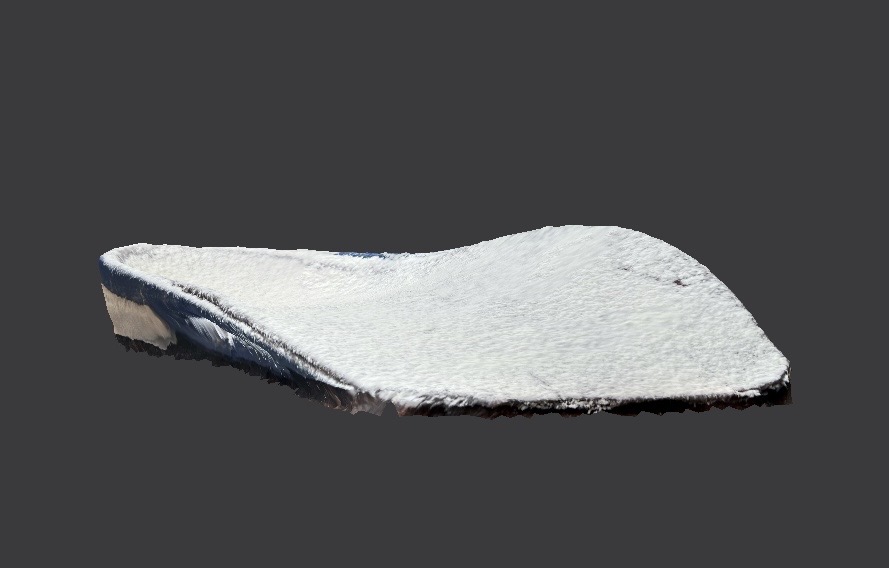
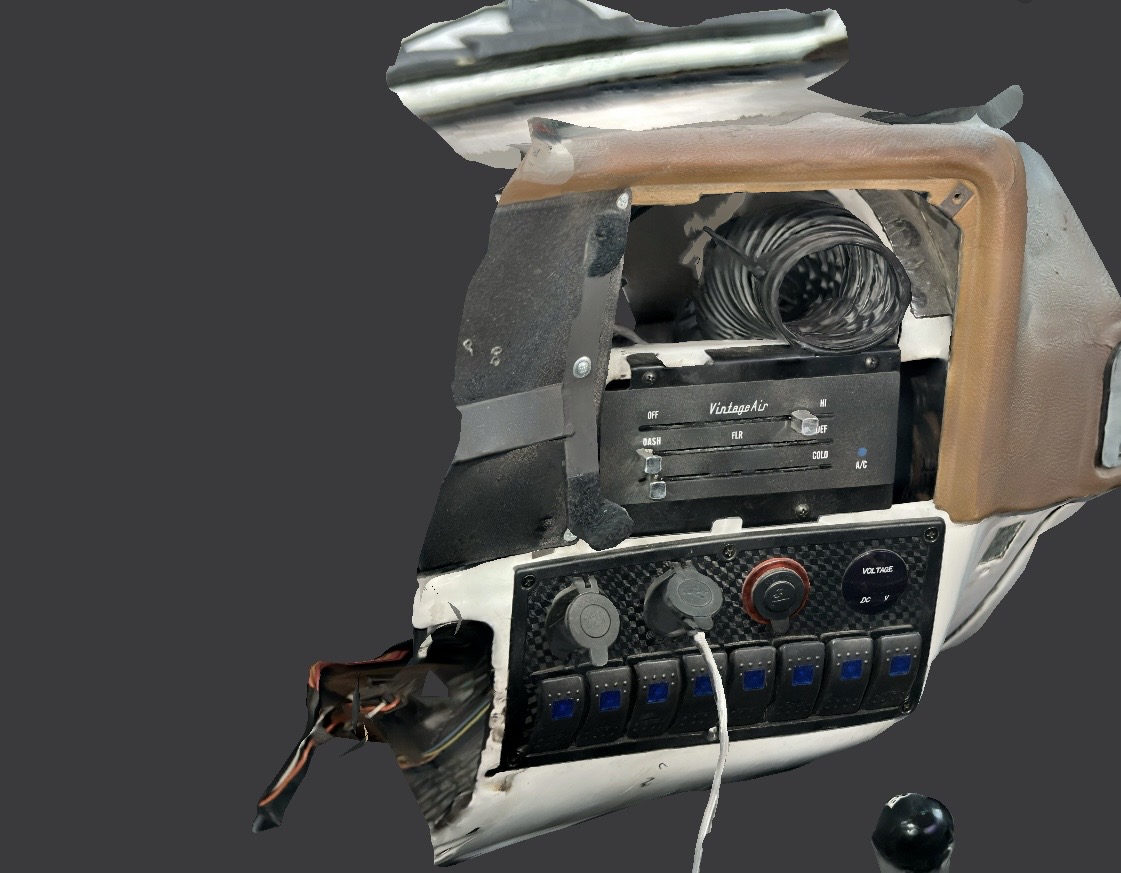
This represents an area we are growing into and plan to do more work. With modern 3D scanning you can retain 99.9% of the detail and dimensional accuracy of a machine or product with the ability of fitting all that reference data on a flash drive. All holes, offsets and features of a physical project are retained as if you are standing there in person with the equipment. This allows us to start to finish design solutions for many problems with the most minimal revisiting and intervention as we have the existing setup right in front of us. We have had incredible success with small and medium sized projects. If you desire machine modifications or machine retrofits let us know. We can bring serious scanners and get you the detail you need for whatever application you may have.
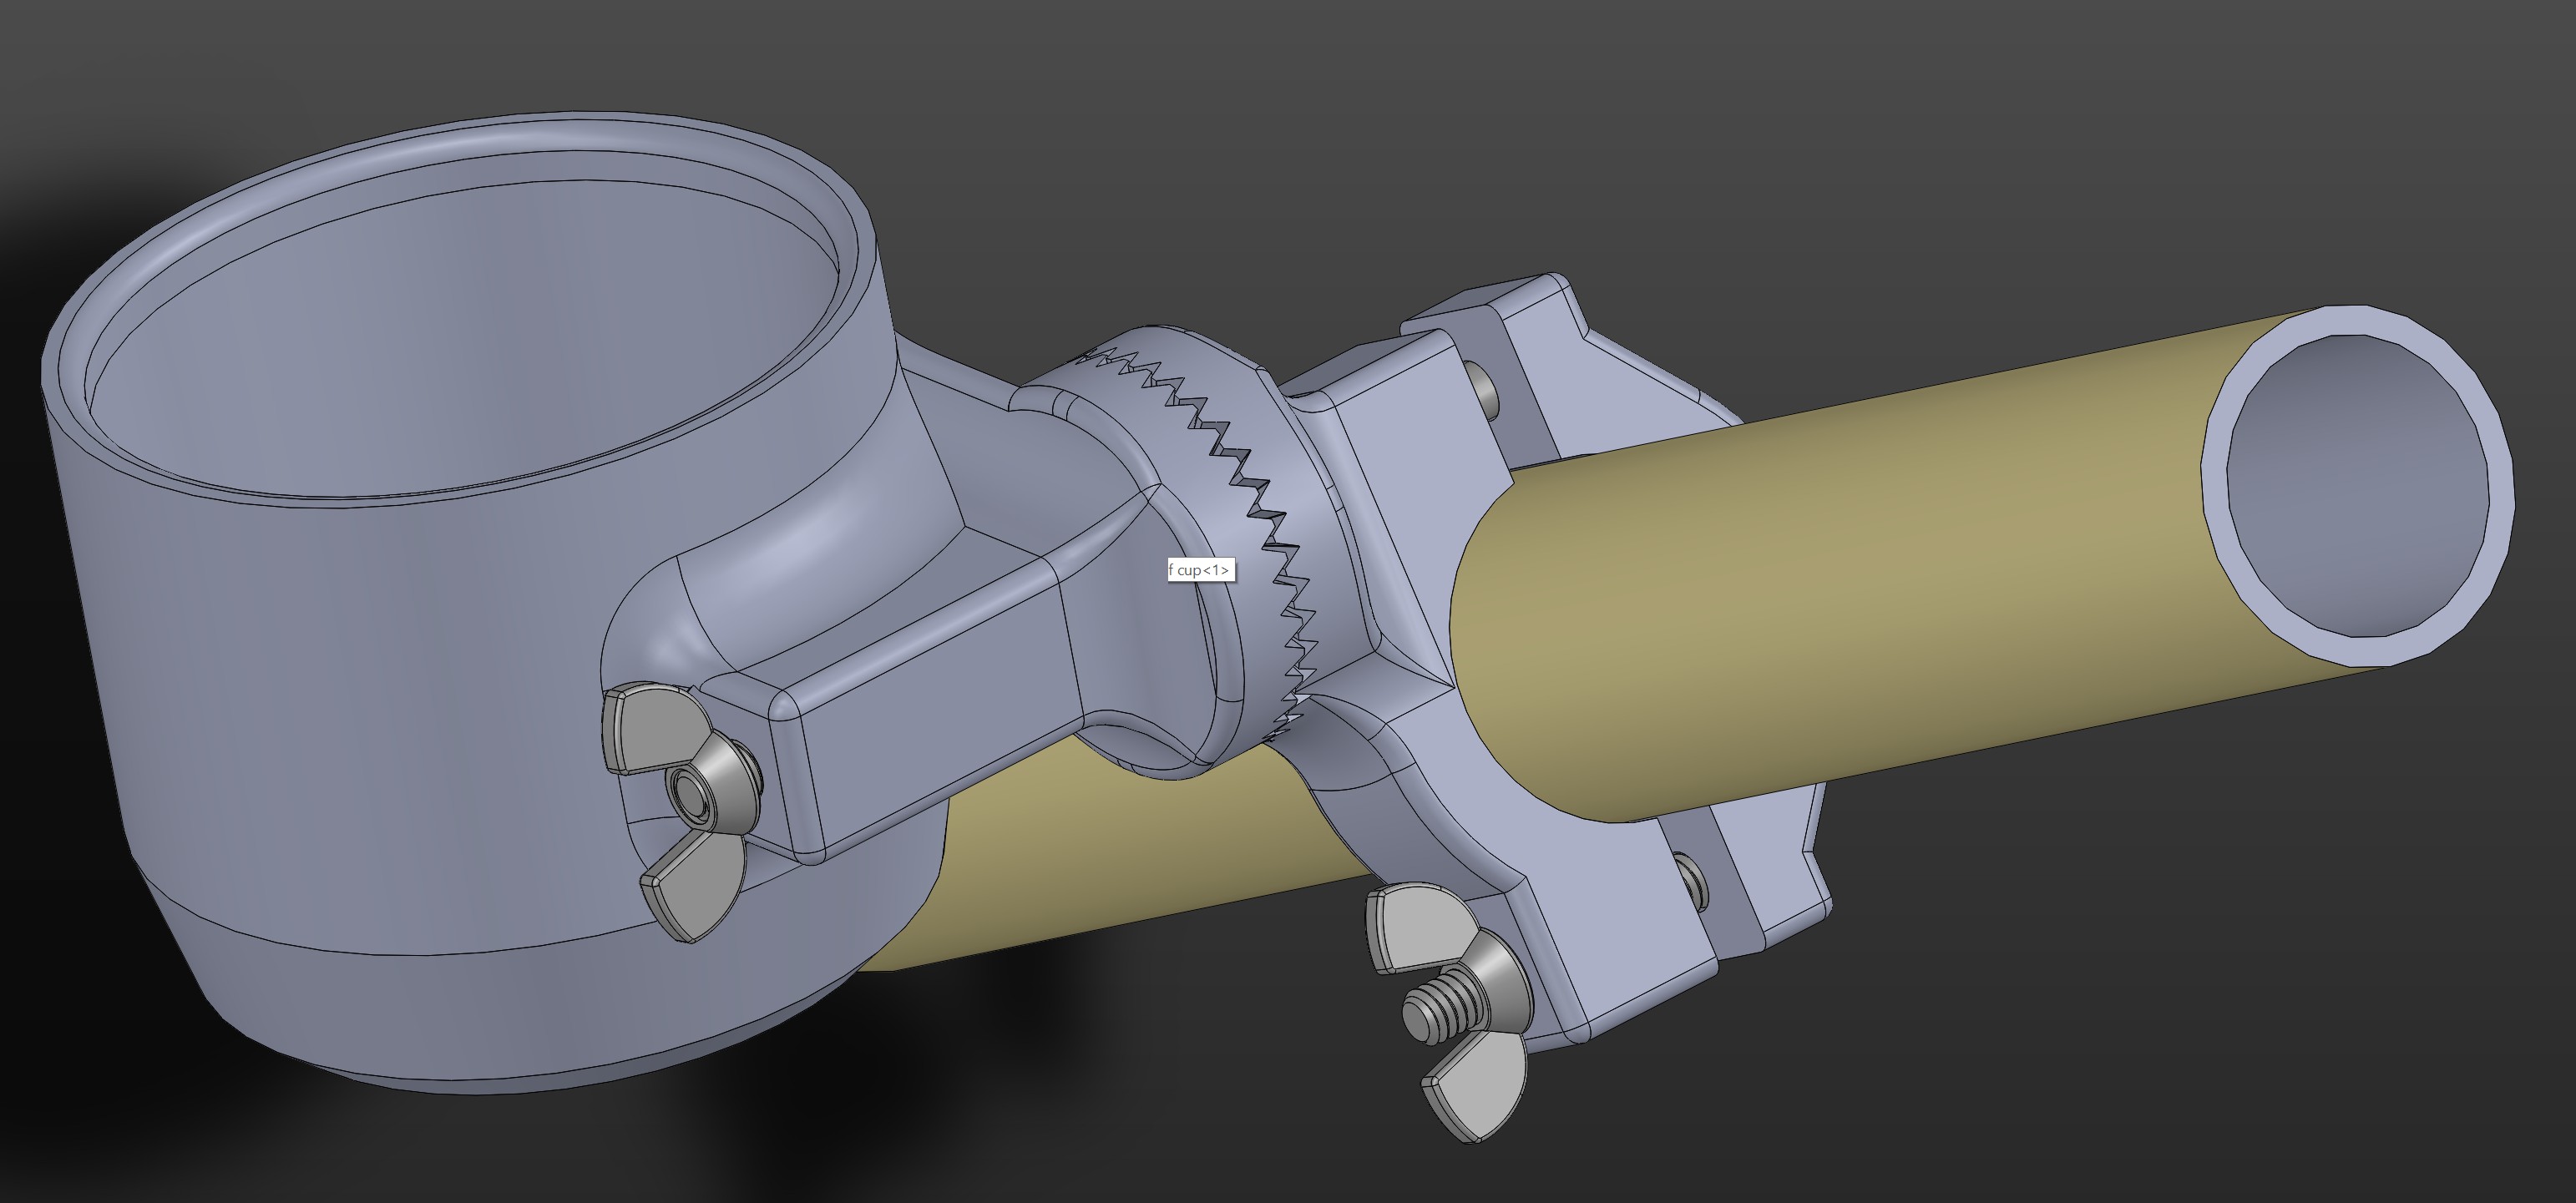
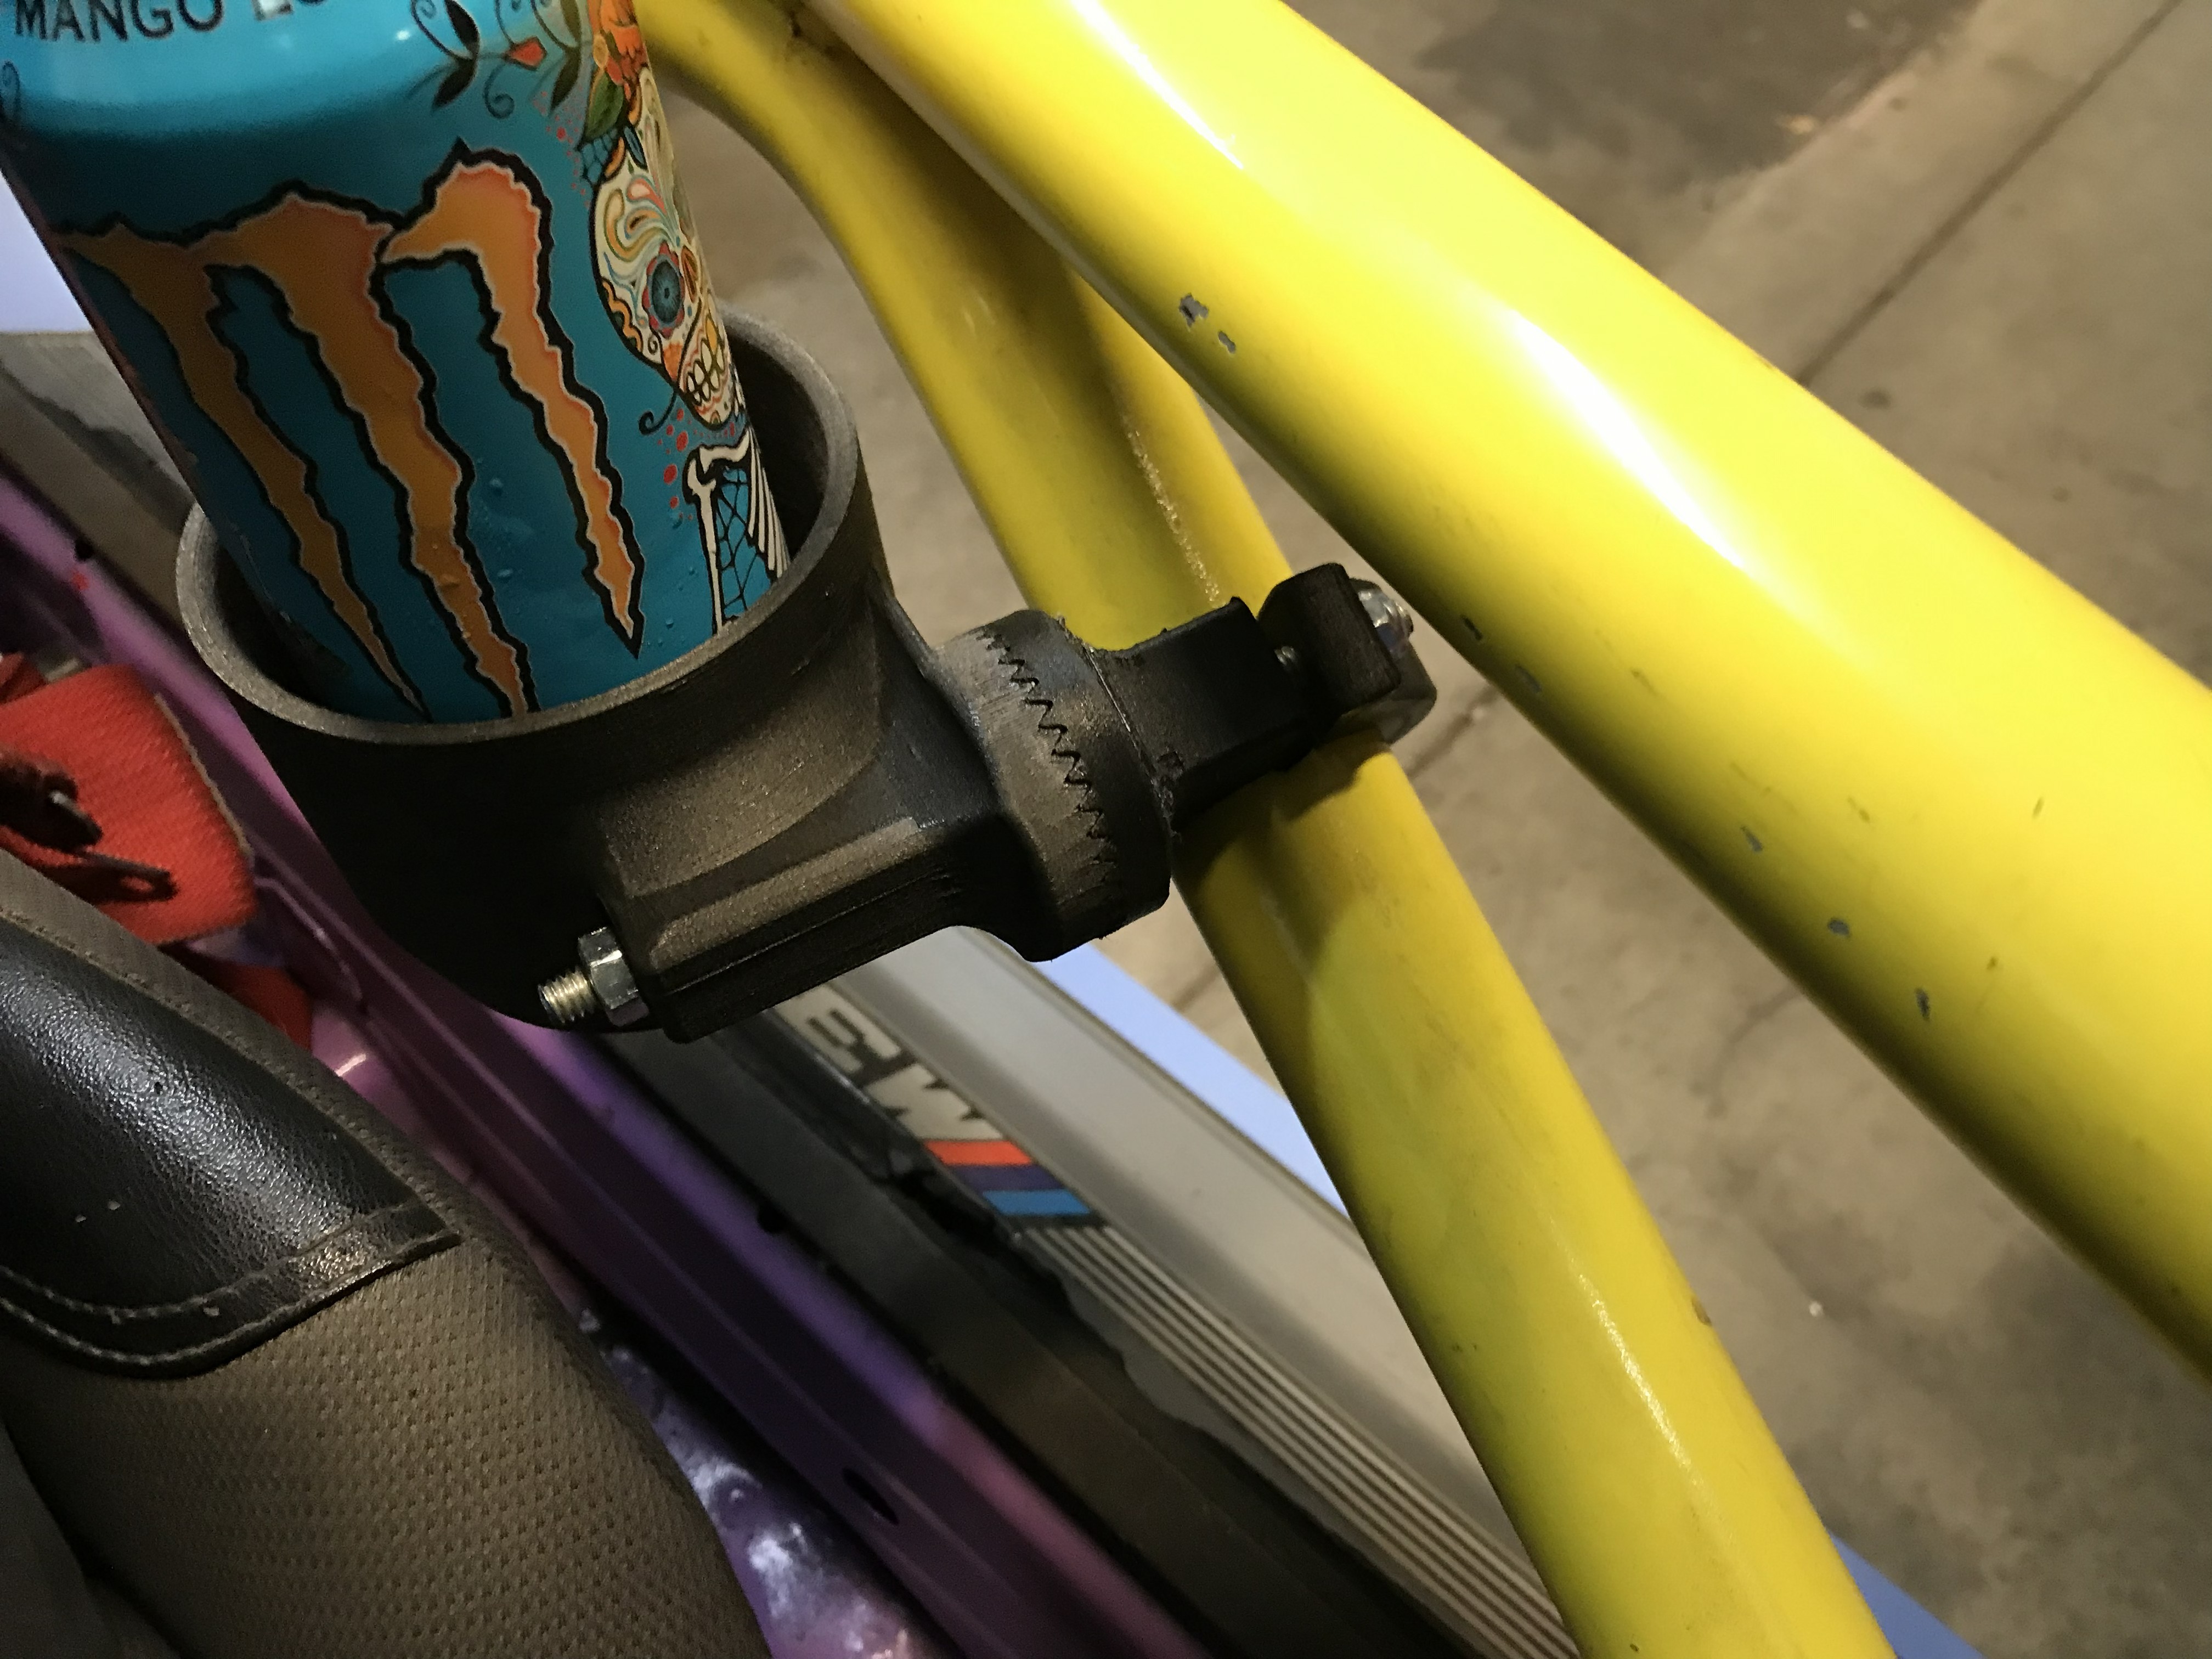
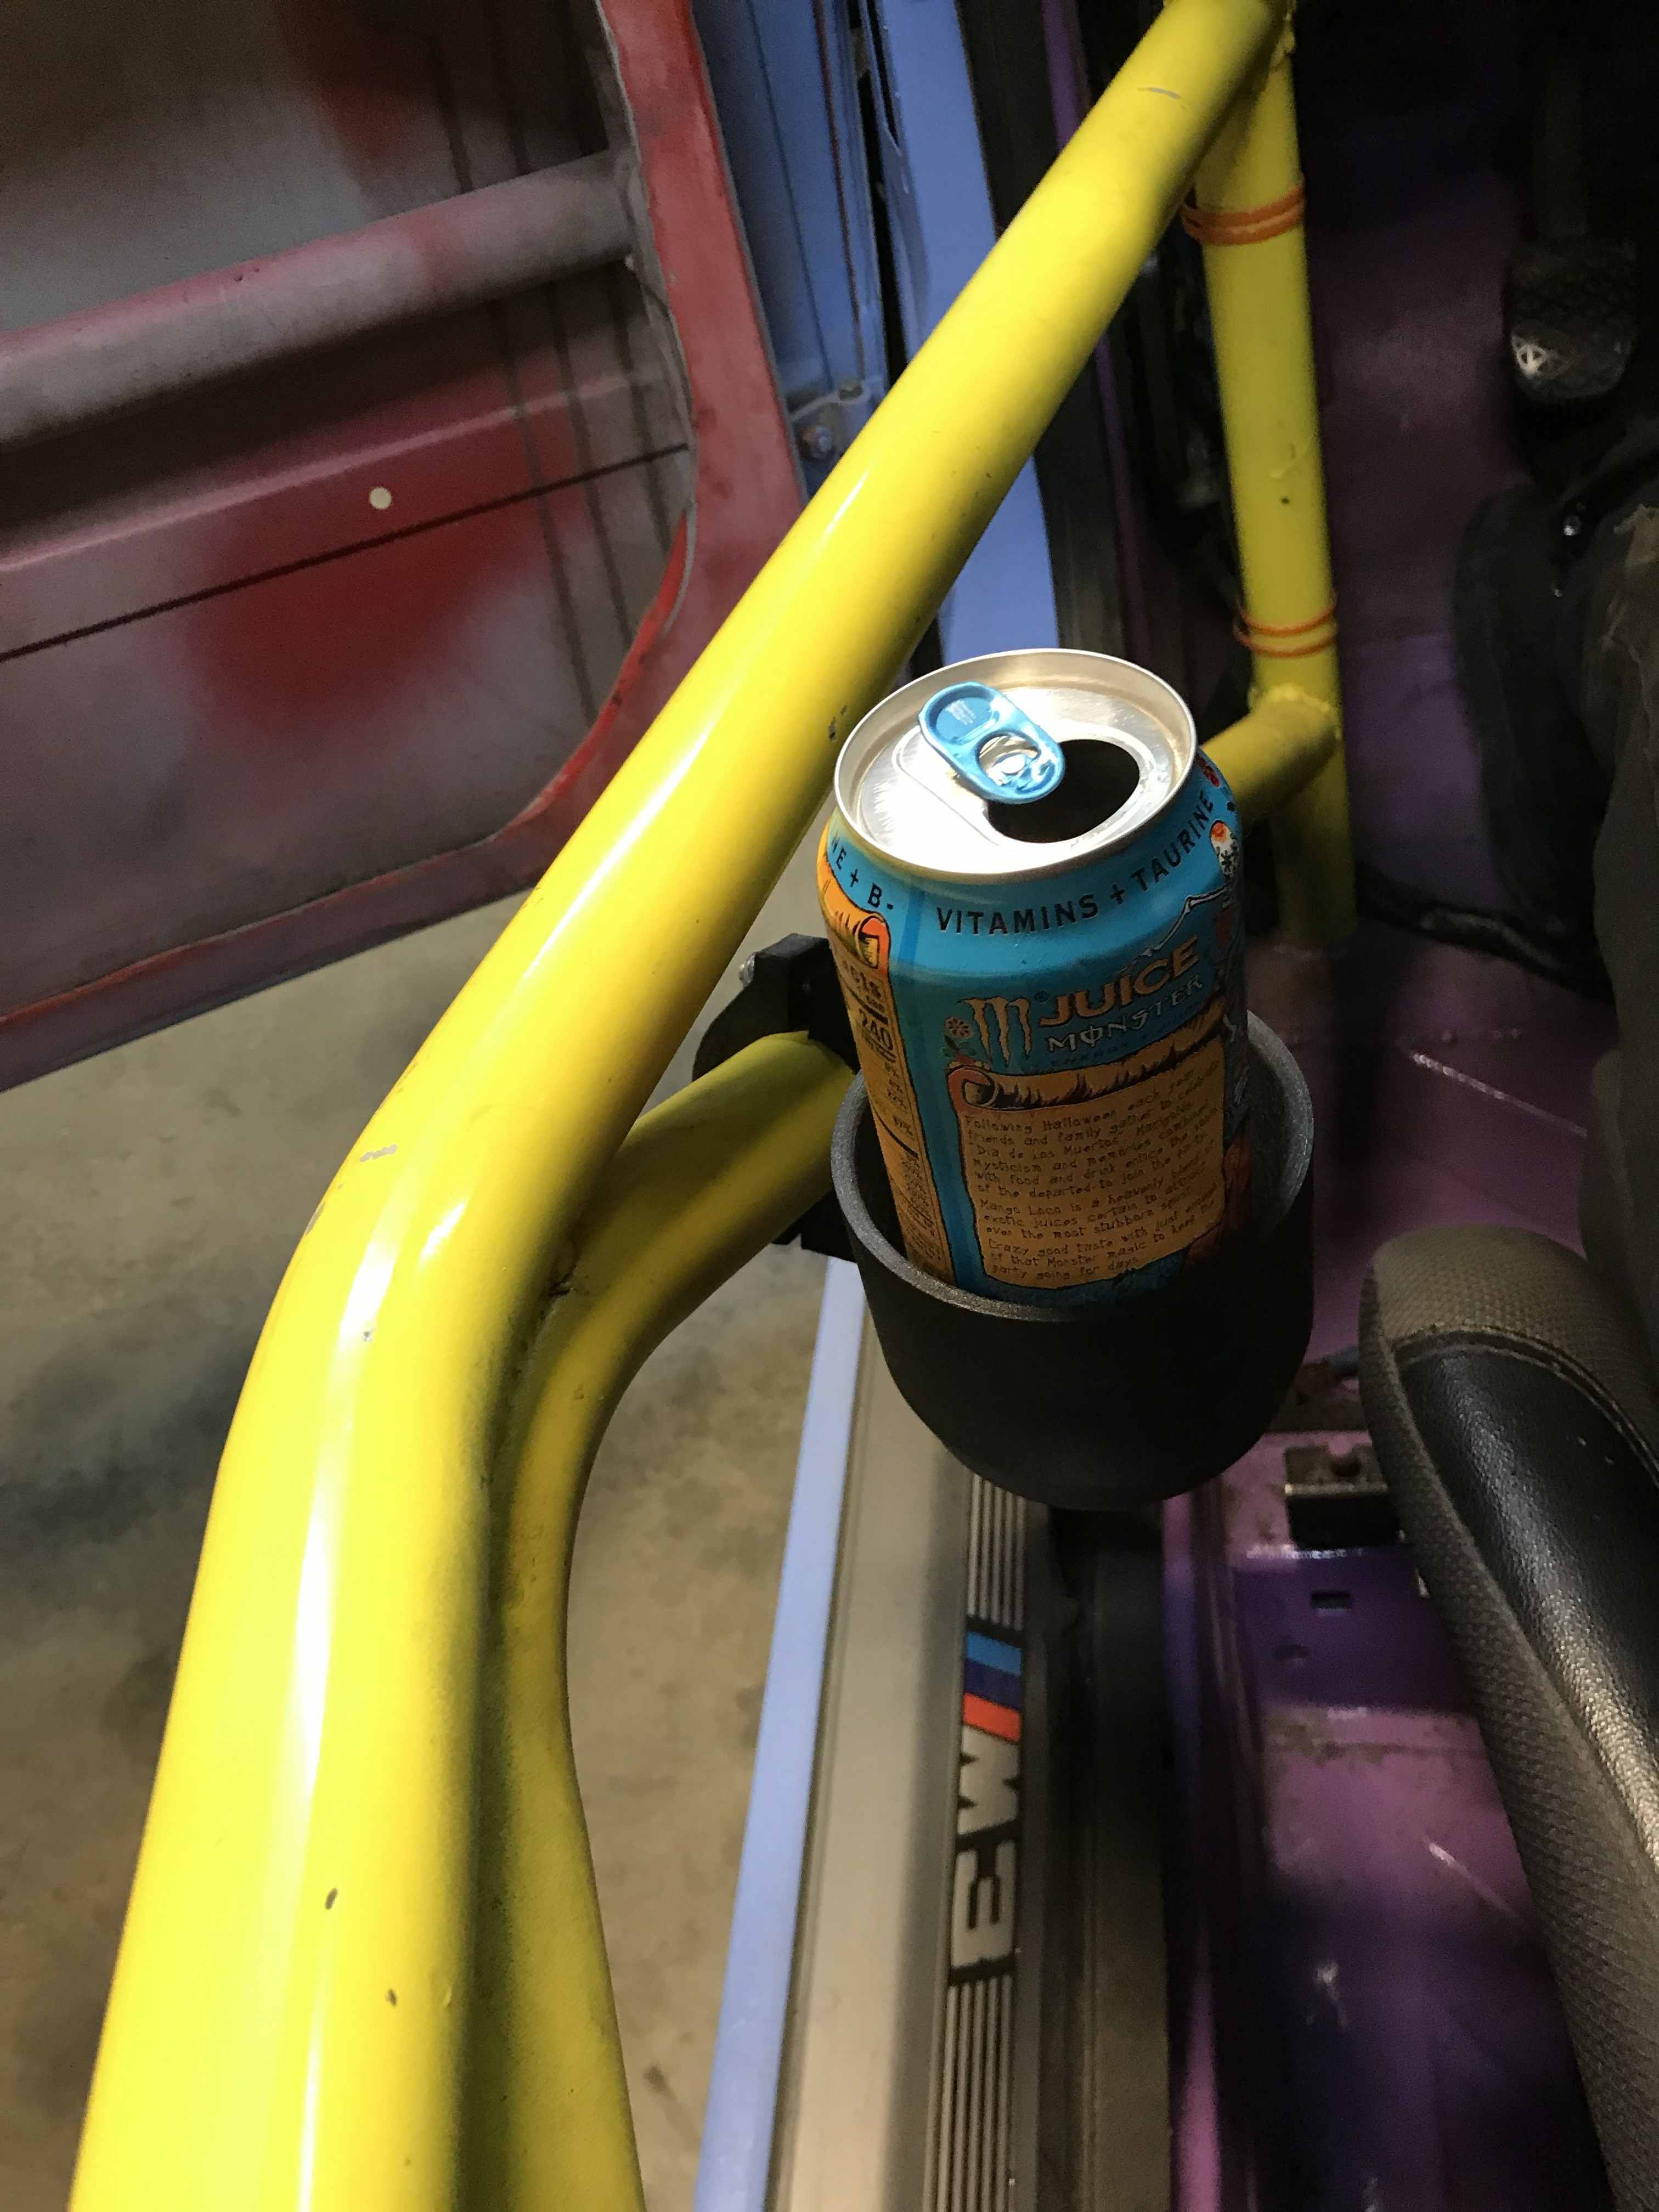
An indexable cage mounted cup holder in a drift car? Yes. No job to big, small, or obscure for us to print. We can print your prototypes or batches of finished product if you are a growing retail company selling end use products right off our machines. We support almost all materials in the engineering world for end use parts except materials from the PEEK/PEKK family of thermoplastics.
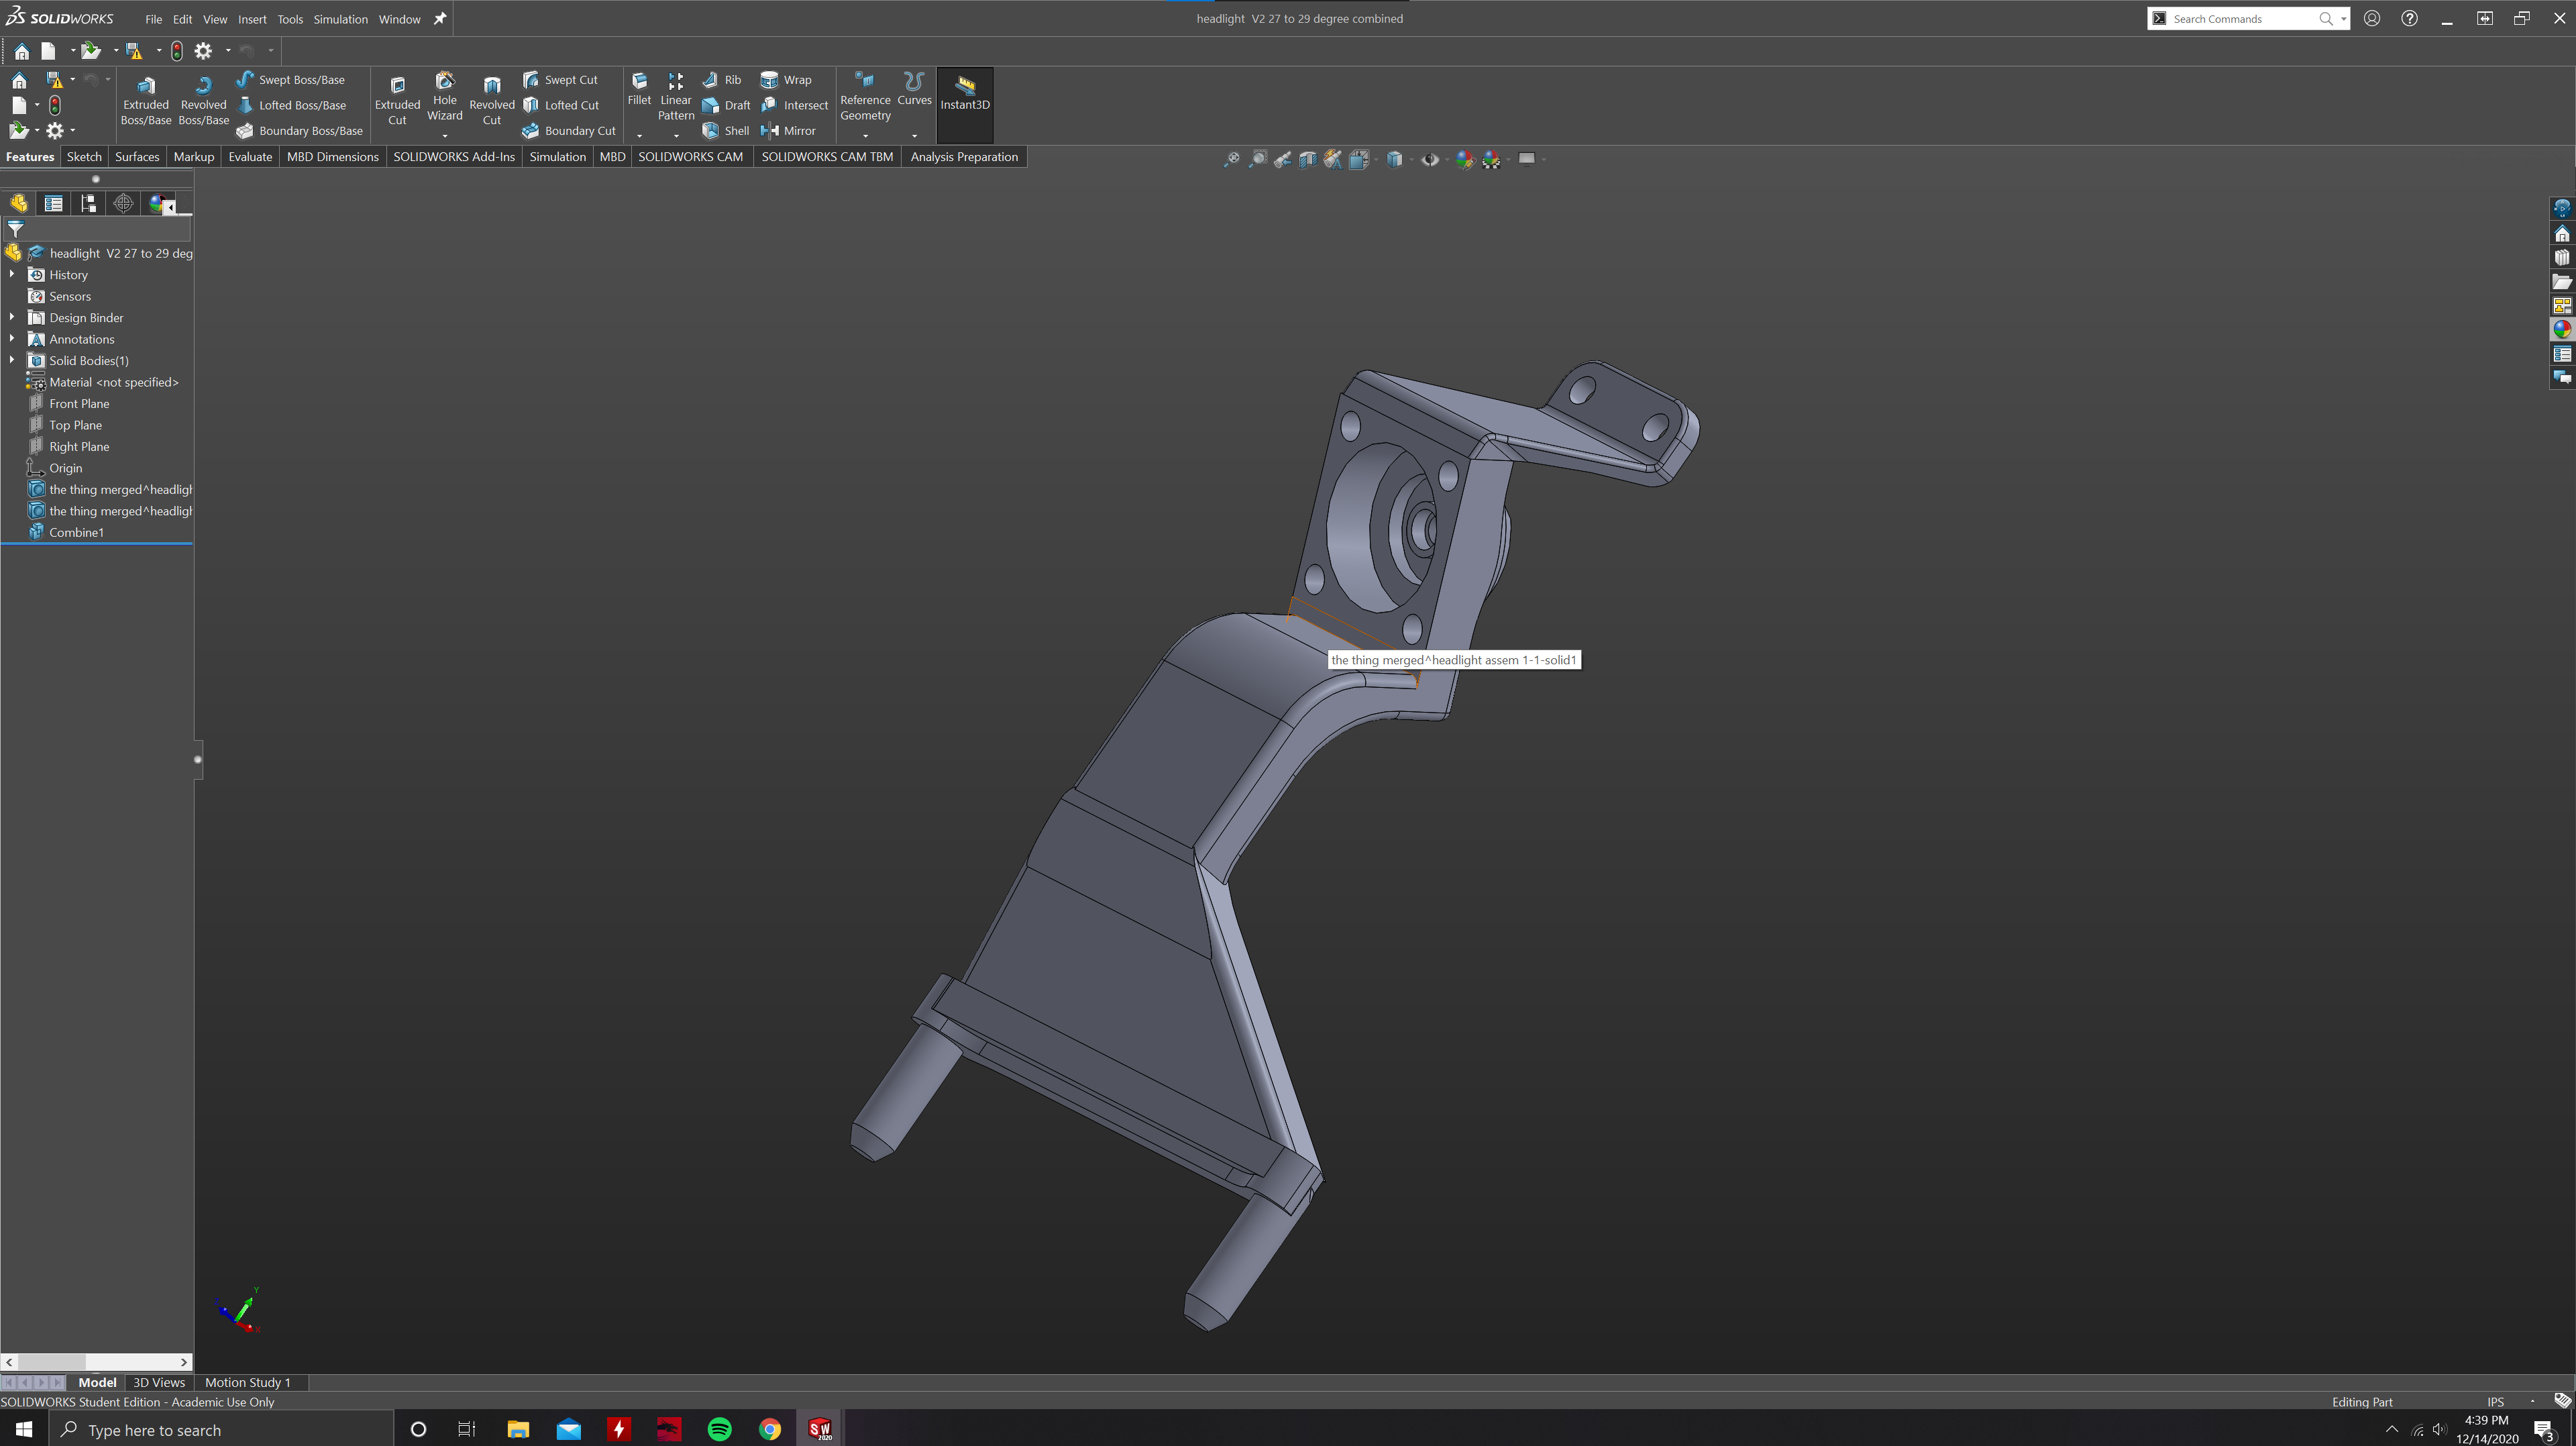
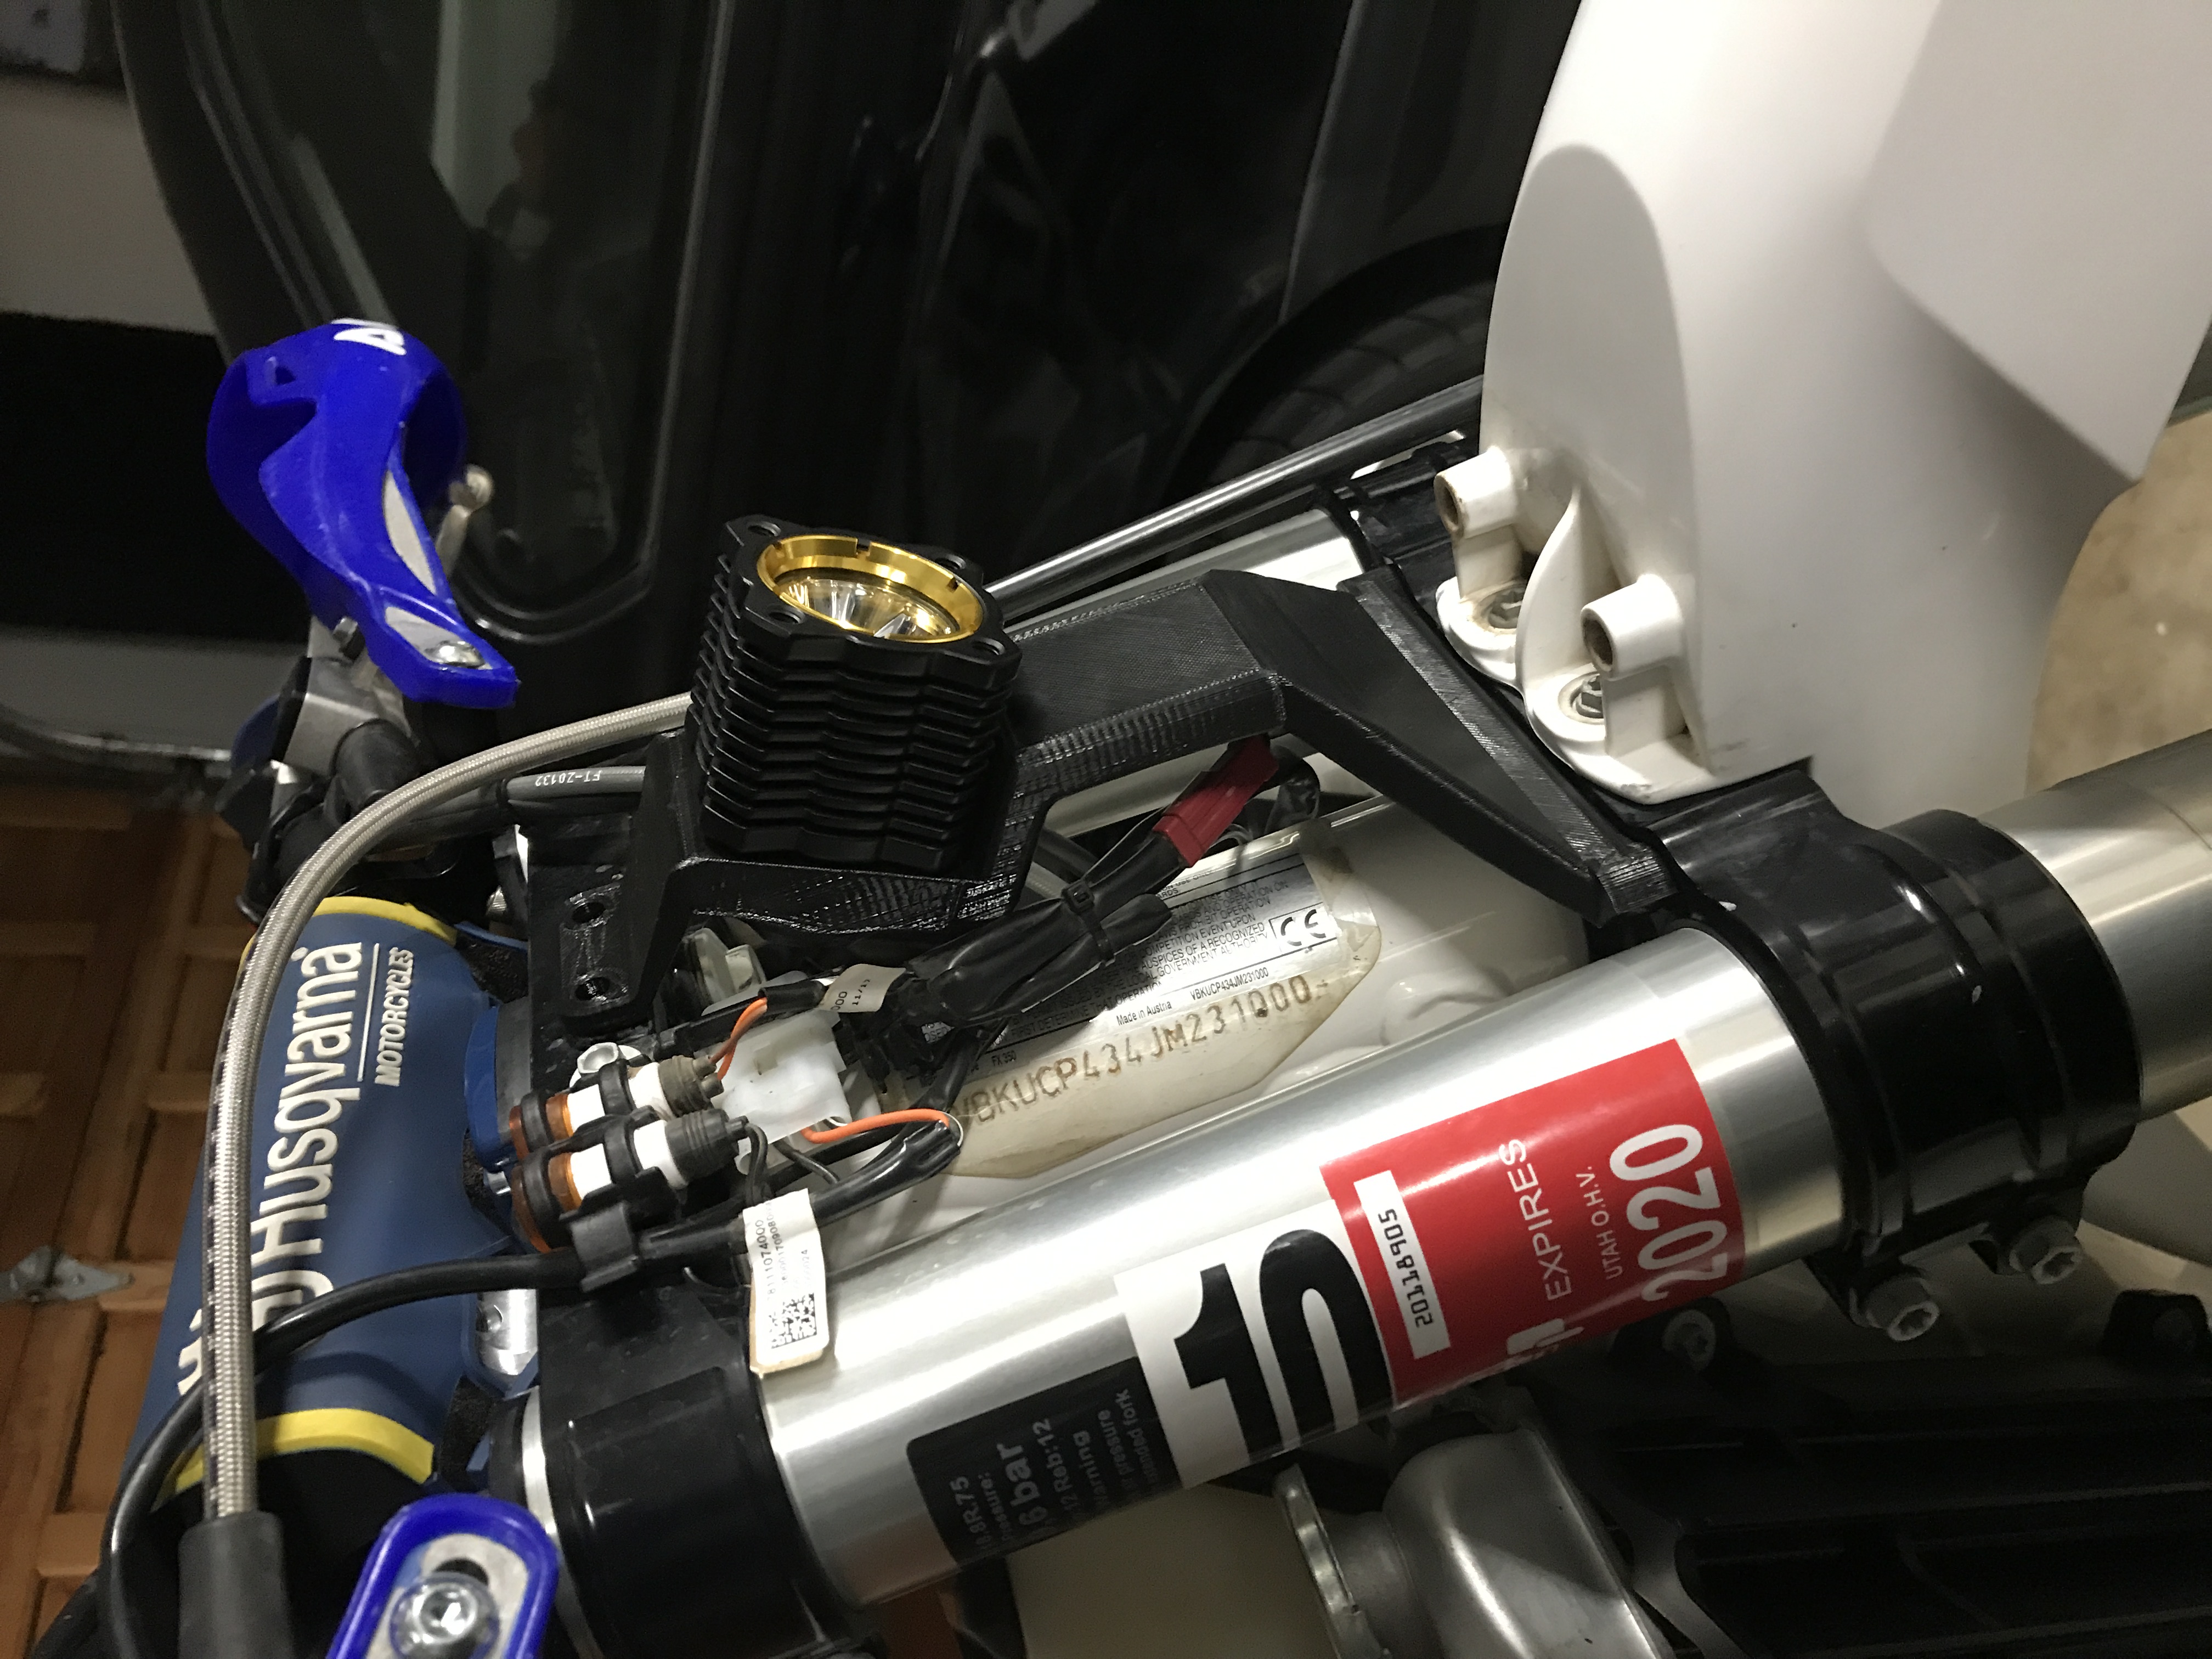
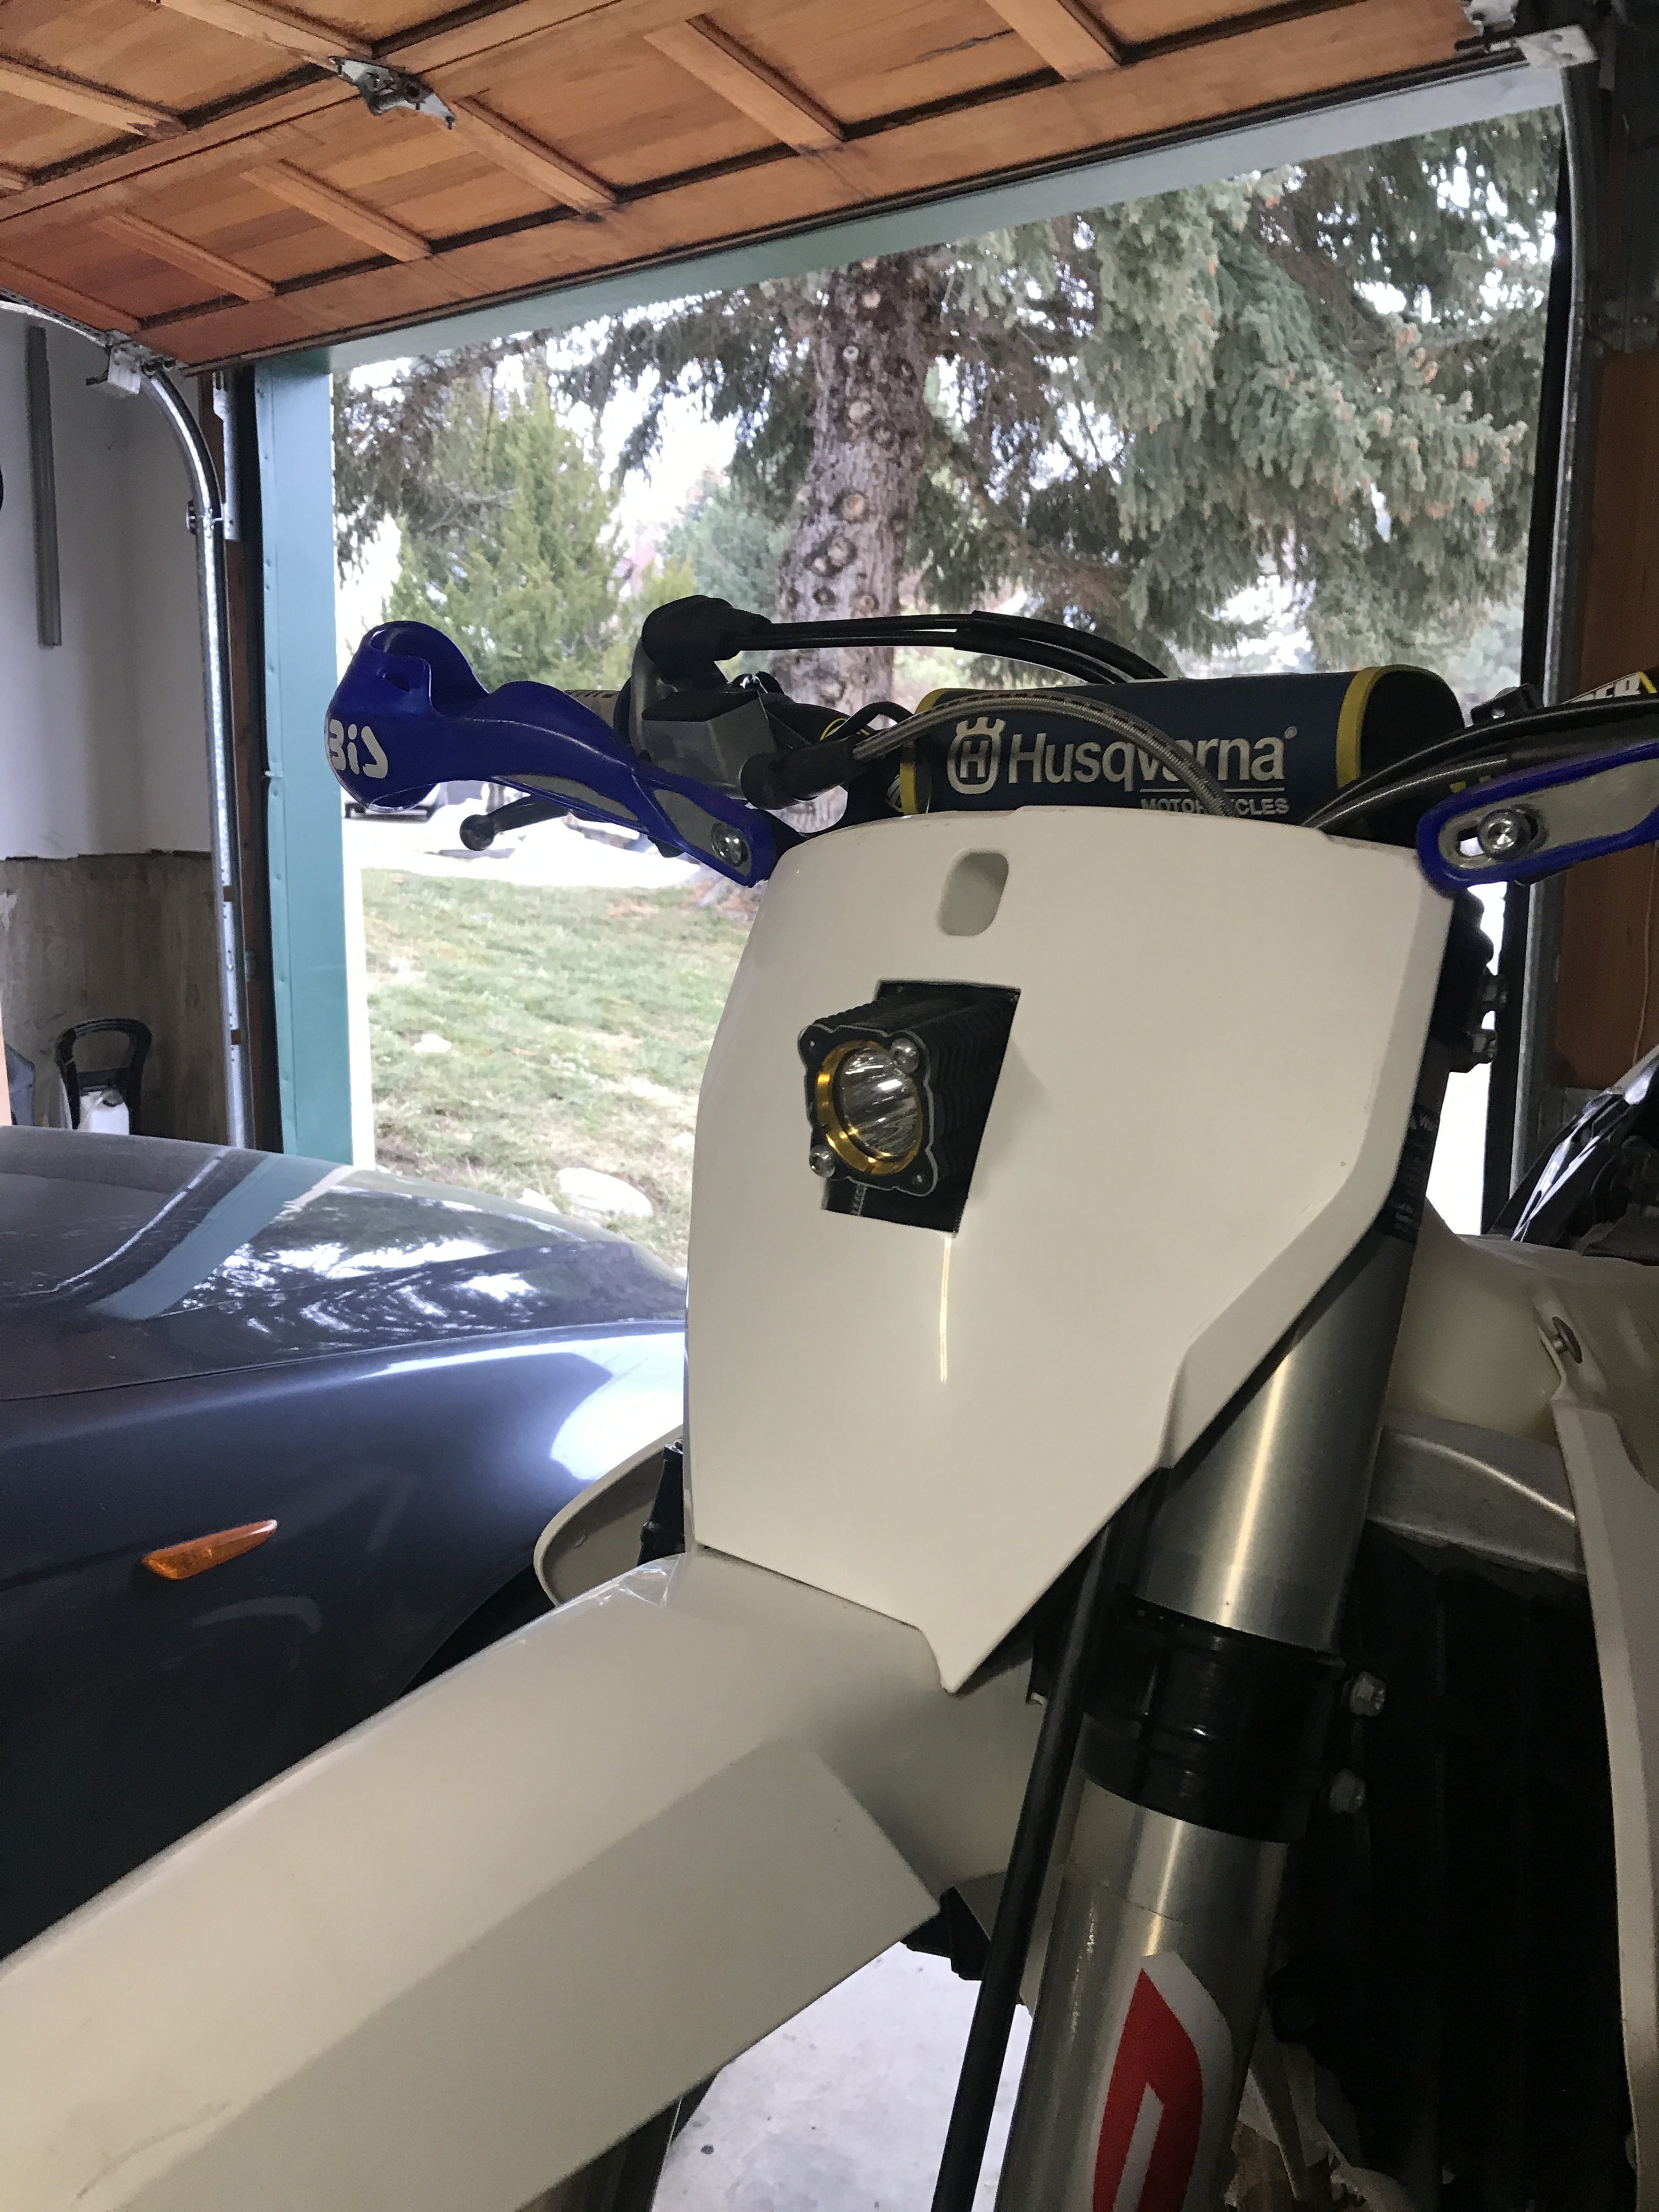
The goal here was to print a headlight system for a enduro bike application that beat the brightness, beam pattern, energy consumption, fit and finish, and price of the OE KTM headlight option. We succeeded by using a KC sourced offroad light and adapted it to the OEM available mounts using a low carbon fill cf-nylon to maintain as much impact resistance as possible. The entire system fits behind the OEM numberplate that gets re-installed with a relief cut as pictured. There is no drilling, tapping, or modifying the bike in any way to accept this modification other than the number plate cut.